Textile Science & Blends
Engineered polyester-spandex and nylon-elastane substrates optimized for 4-way stretch recovery, thermal regulation, and durability.
How global sportswear brands, athletic federations, and high-growth fitness labels scale high-compression, moisture-wicking activewear lines with zero-defect quality control and factory-direct pricing.
Engineered polyester-spandex and nylon-elastane substrates optimized for 4-way stretch recovery, thermal regulation, and durability.
Over two decades of compliant supply chain execution, exporting structured apparel lots across North America, Europe, Australia, and Asia.
Dedicated cutting, flatlock stitching, sublimation printing, and seam-sealing units supported by 100+ industrial specialized machines.
Strict ASTM D3786 burst strength and AATCC moisture-wicking testing protocols applied inline from pattern grading to final packing.
In the modern technical activewear ecosystem, procurement directors face a recurring dilemma: balancing ultra-durable elastomeric recovery with lightweight breathability while maintaining seamless scalability.
Standard activewear often fails under high-velocity athletic movement—experiencing seam popping, fabric sheer transparency during squat-tests, and color degradation under heavy friction. At Sedate Group of Industries, our Performance Training Apparel OEM platform addresses these systemic structural vulnerabilities through specialized yarn selection, ergonomic paneling, and locked-in tech-pack specifications.
Whether manufacturing elite compression rash guards, heavy-duty gym apparel, or multi-directional fight shorts, our Sialkot manufacturing hub integrates end-to-end production control. We remove middle-tier markup risks and deliver true technical value to global distributors and direct-to-consumer athletic brands.
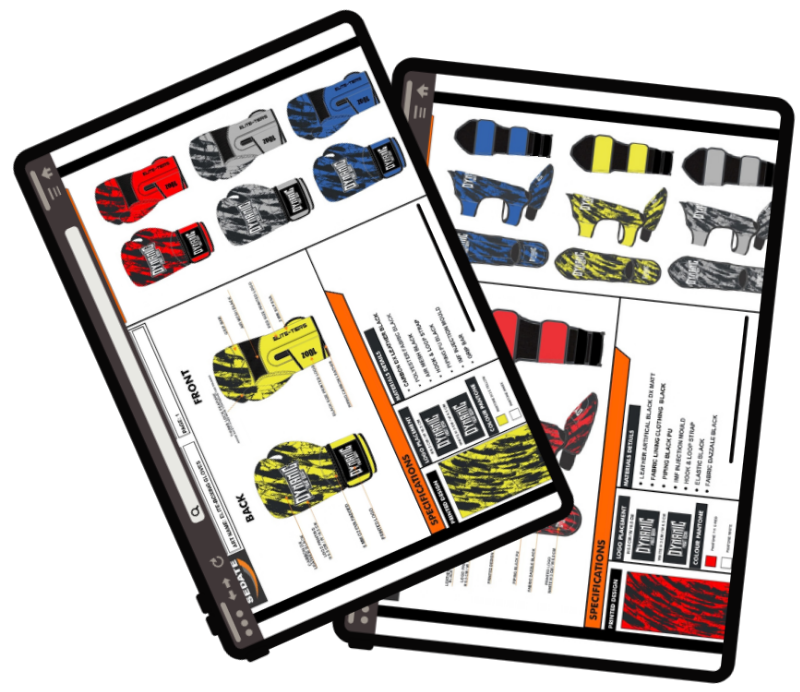
Below is an authoritative technical matrix comparing industry standard apparel vs. Sedate Group's OEM engineering specs for performance training apparel:
| Technical Metric | Standard Commercial Market | Sedate Group OEM Specification | Performance Advantage |
|---|---|---|---|
| Fabric Density (GSM) | 140 - 180 GSM Single Knit | 220 - 340 GSM High-Gauge Warp Knit | Zero sheer transparency, superior squat-proof opacity, structural endurance. |
| Fiber Composition | 100% Basic Polyester | 82/18 Poly-Elastane or 75/25 Nylon-Spandex | Multi-directional 4-way stretch with over 98% elastic recovery retention. |
| Seam Construction | Standard Overlock (ISO 504) | ISO 4915 Type 607 Flatlock (4-Needle 6-Thread) | Flat, chafe-free contact against skin; 45% higher tensile seam strength. |
| Moisture Management | Topical Chemical Spray finish | Yarn-Level Micro-Groove Hydrophilic Wicking | Permanent moisture dispersion across washing cycles (AATCC 195 compliance). |
| Color Fastness | Surface Transfer Printing | 210°C Italian Ink High-Pressure Sublimation | No color bleeding, peeling, or ghosting under intense abrasion and sweat. |
Engineered to rigid technical standards, our OEM product categories support full private label customisation, custom sizing charts, tailored branding trims, and custom tech-pack developments.
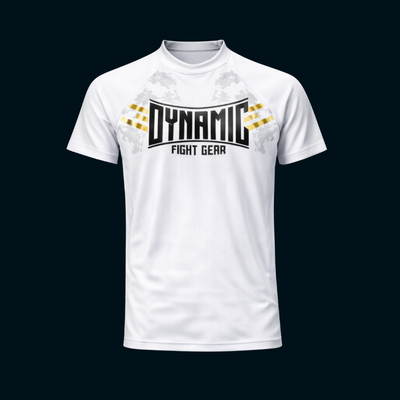
230–260 GSM polyester-spandex blend with anti-microbial treatment, 4-way stretch flex panels, and high-density flatlock stitching for combat sports and cross-training.
Technical Specs →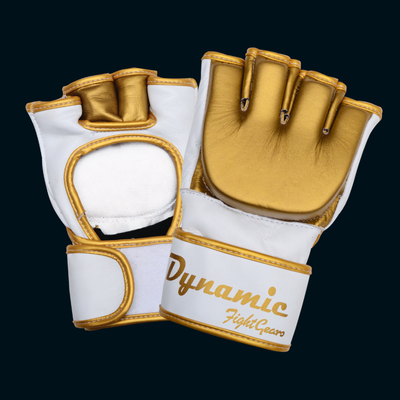
Lightweight 160 GSM micro-ripstop synthetic fabric with 4-way elastane crotch gussets, reinforced side slits, and non-slip silicone inner waistband tape.
Technical Specs →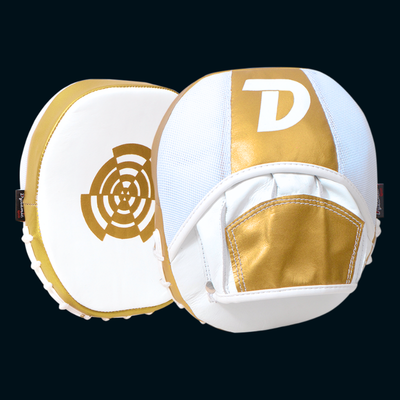
280–320 GSM heavy compression nylon-spandex interlock, delivering targeted 15–20 mmHg graduated muscle stability to reduce fatigue during high-load workouts.
Technical Specs →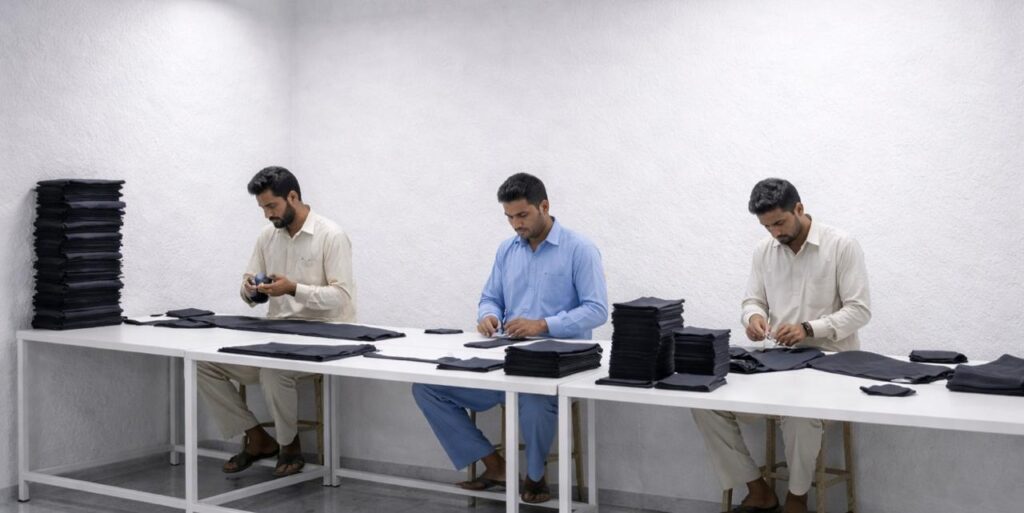
340 GSM cotton-poly French terry and heavy tech-fleece outerwear featuring double-lined storm hoods, waterproof zip enclosures, and athletic raglan sleeves.
Technical Specs →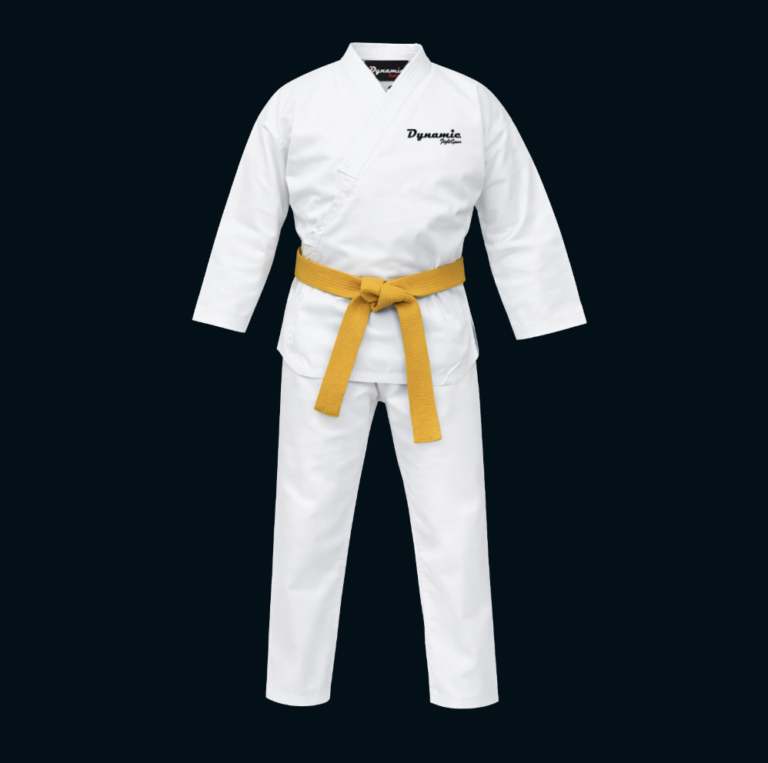
Heavyweight grappling tops and rash guards crafted to fit beneath martial arts gis, featuring reinforced neck collars and friction-resistant elbow zones.
Technical Specs →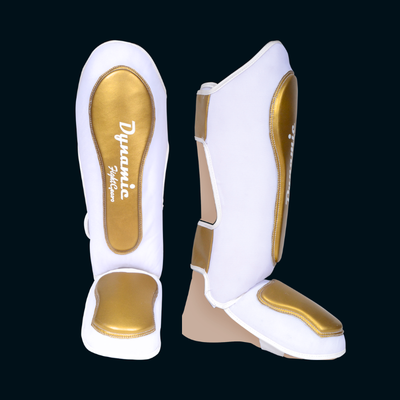
Integrated high-density EVA shock cell pads positioned over vital muscle areas, wrapped in 4-way moisture-dispersing compression fabric.
Technical Specs →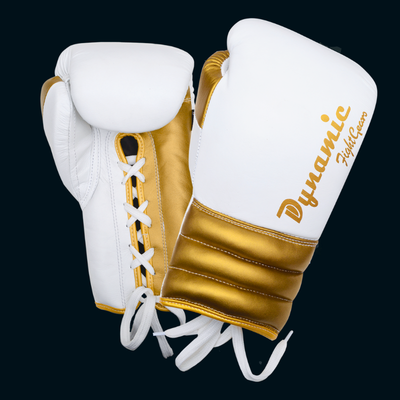
Complemented by matching fight accessories, hand wraps, and conditioning gear to offer cohesive private label product bundles for combat brands.
Technical Specs →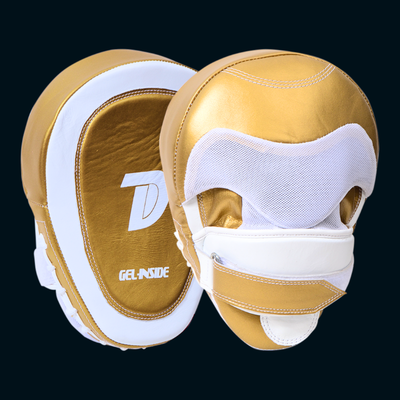
Heavy-duty, weather-resistant activewear tops, moisture-managing polo shirts, and track jackets engineered for athletic coaches and corner staff.
Technical Specs →Global sportswear buyers and supply chain executives must adapt to rapid technological evolutions. Here are the pivotal micro and macro trends reshaping OEM activewear sourcing over the next decade.
Modern athletic consumers demand circular sustainability without sacrificing compression performance. OEM sourcing is rapidly shifting from virgin polyester to Global Recycled Standard (GRS) certified Repreve® recycled yarns derived from post-consumer ocean plastics.
Sedate Group is actively integrating recycled polyester-elastane blends into our activewear lines. These sustainable substrates maintain identical burst strength, moisture dispersion rates, and tensile elasticity as traditional synthetic yarns.
Generic single-panel compression is obsolete. Global brands are ordering performance garments engineered with multi-zone variable compression (10 mmHg to 22 mmHg). By placing micro-ribbed paneling along key muscle groups (quadriceps, hamstrings, and deltoids), garments provide targeted venous return assistance and reduce DOMS (Delayed Onset Muscle Soreness).
To eliminate chafe points entirely and minimize fabric scrap waste during cutting, seamless circular knitting is becoming a baseline industry requirement. By engineering functional ventilation mesh directly into the weave, brands reduce sewing labor costs while creating superior aesthetic paneling.
Global regulatory frameworks (such as EU REACH and US EPA guidelines) are banning fluorinated DWR chemical treatments. Next-generation performance apparel utilizes plant-derived or silicone-based hydrophobic finishes alongside silver-ion antimicrobial treatments to prevent odor-causing bacterial growth in synthetic fibers.
How engineering choices at the prototype phase dictate commercial margins, return rates, and end-user loyalty in the competitive activewear marketplace.
Developing market-leading performance training apparel requires seamless synergy between textile chemistry and garment construction. Key industry innovations include:
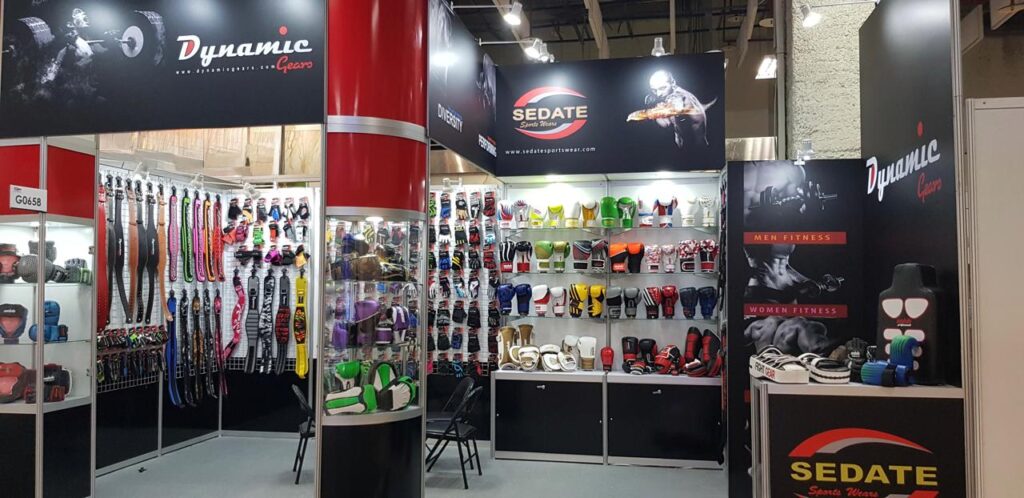
Established in 2002 in Sialkot, Pakistan—the globally recognized pinnacle of hand-crafted and technical sporting goods manufacturing—Sedate Group of Industries provides true vertical integration for OEM clients.
Unlike trading entities or unverified intermediaries, our facility operates 4 dedicated manufacturing divisions: Sedate Enterprise, Sedate Sportswear, Dynamic Gear, and Dynamic Fightgear. We manage over 200 skilled textile artisans and 100+ specialized machines spanning automated cutting, heavy-duty stitching, dye sublimation, and inline testing.
With an active export footprint spanning 20+ countries—including established distribution channels across the United States, United Kingdom, Canada, Germany, Spain, Australia, Europe, and the Middle East—we deliver certified quality, reliable 45-day lead times, and factory-direct pricing transparency.
Unified under a single rigorous Quality Management System to cover all fight gear, activewear, and athletic hardware requirements.
Leather goods, combat equipment & professional fight gear
Performance training apparel, activewear & sublimated kits
Fitness accessories, lifting gear & protective wraps
Pro-fight gear, martial arts uniforms & cage equipment
Custom woven tags, heat-seal neck transfers, silicone logo badges, hangtags, and retail polybags.
Flexible MOQs starting at 100 pcs per style with split sizing options to help new brands launch safely.
Rapid pattern development, tech-pack vector grading, and physical sample dispatch via courier.
Transparent FOB, CFR, or DDP pricing with zero intermediary commissions or hidden surcharges.
Four structured phases ensuring every repeat order matches the approved physical sealed sample to exact tolerances.
Our textile engineers evaluate your vector flats, GSM requirements, elastane ratios, and dimensional specs for production feasibility.
We produce physical prototypes, perform stretch-recovery & color-fastness tests, and ship sealed pre-production samples for client sign-off.
Bulk fabric is laser-cut and processed through 4-needle flatlock lines under continuous inline quality control audits.
Carton audit, dimensional check, barcoding, and custom clearance documentation for air, ocean, or express delivery.
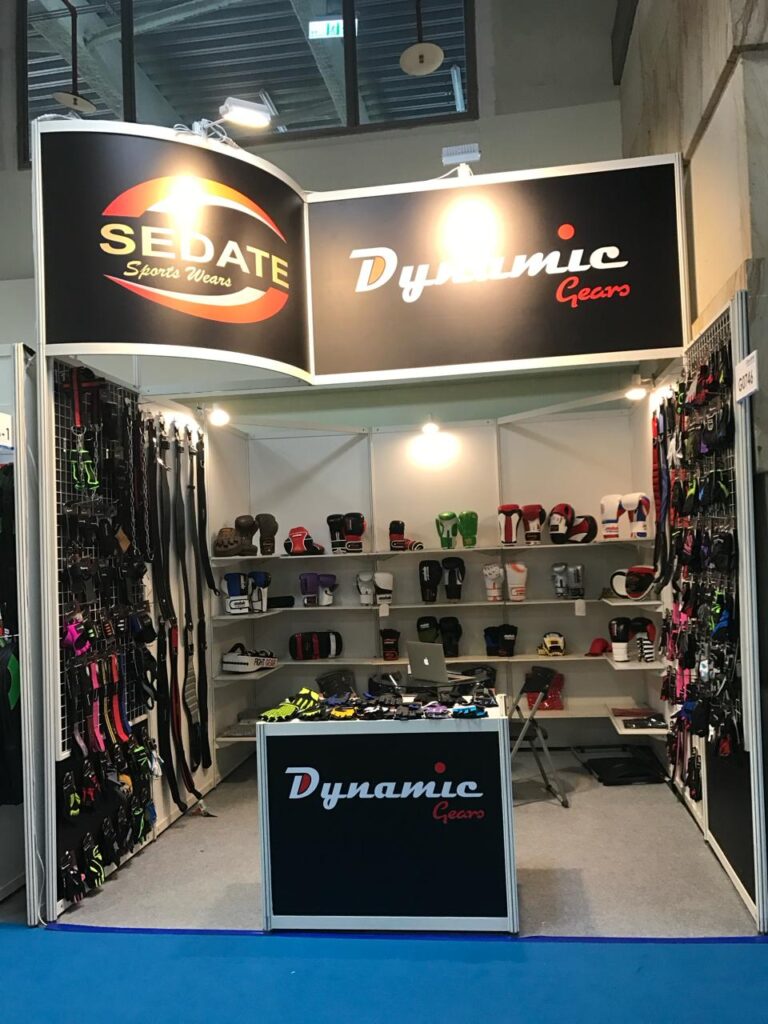
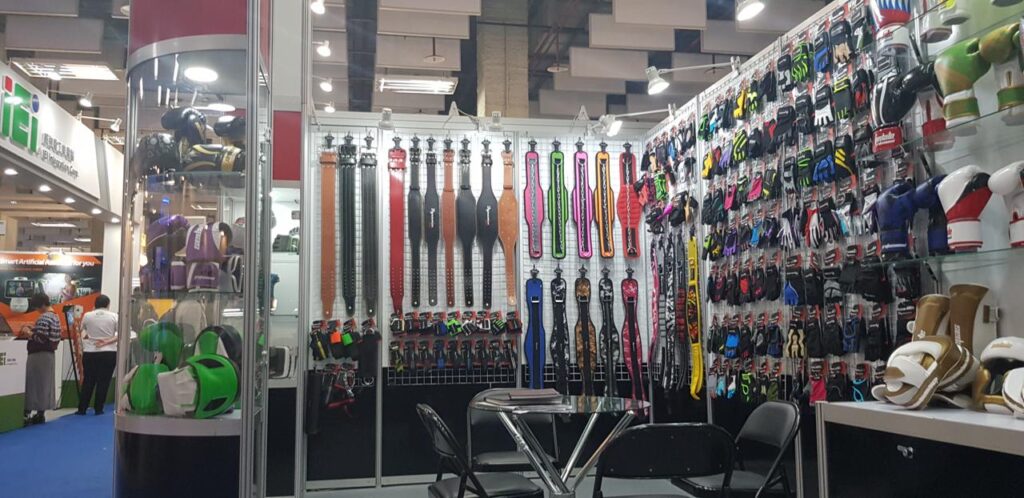
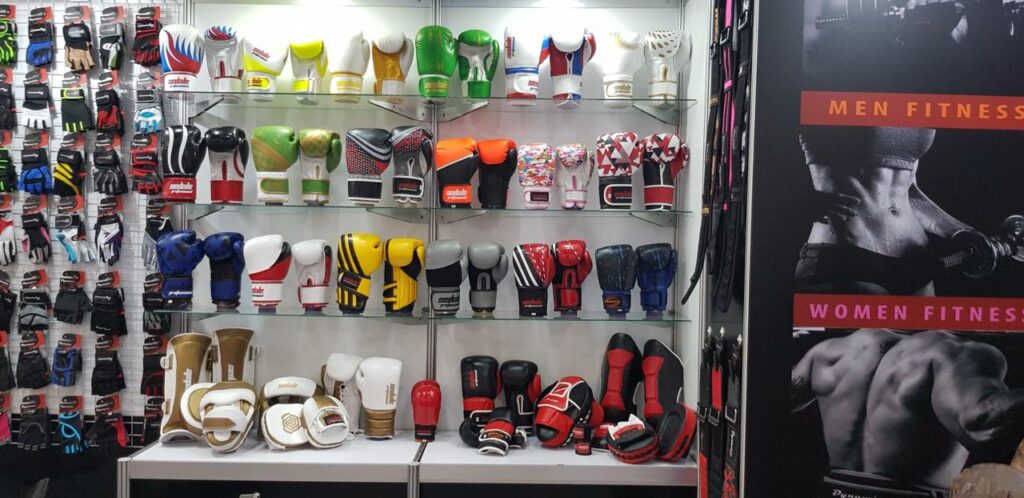
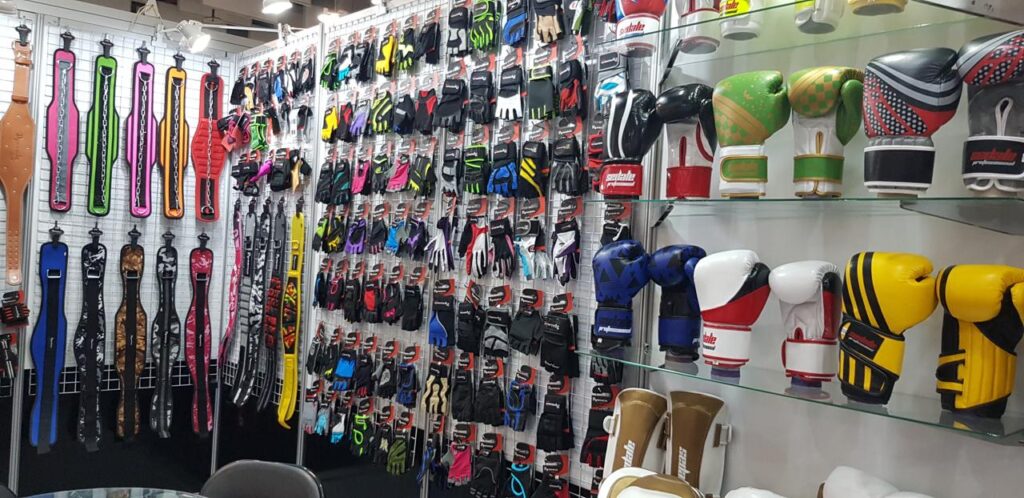
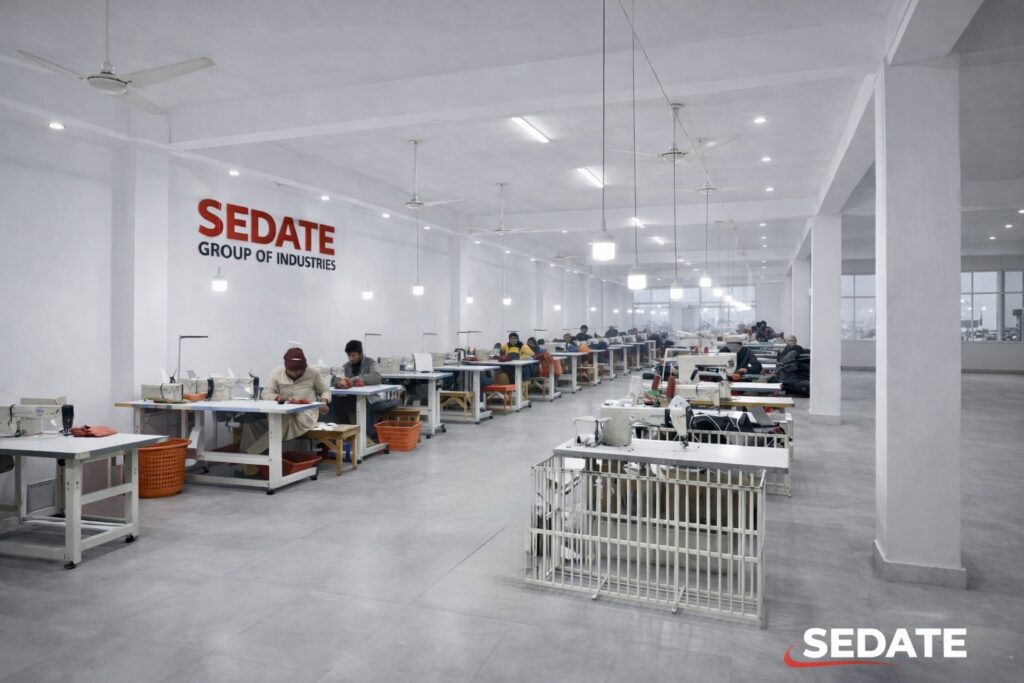
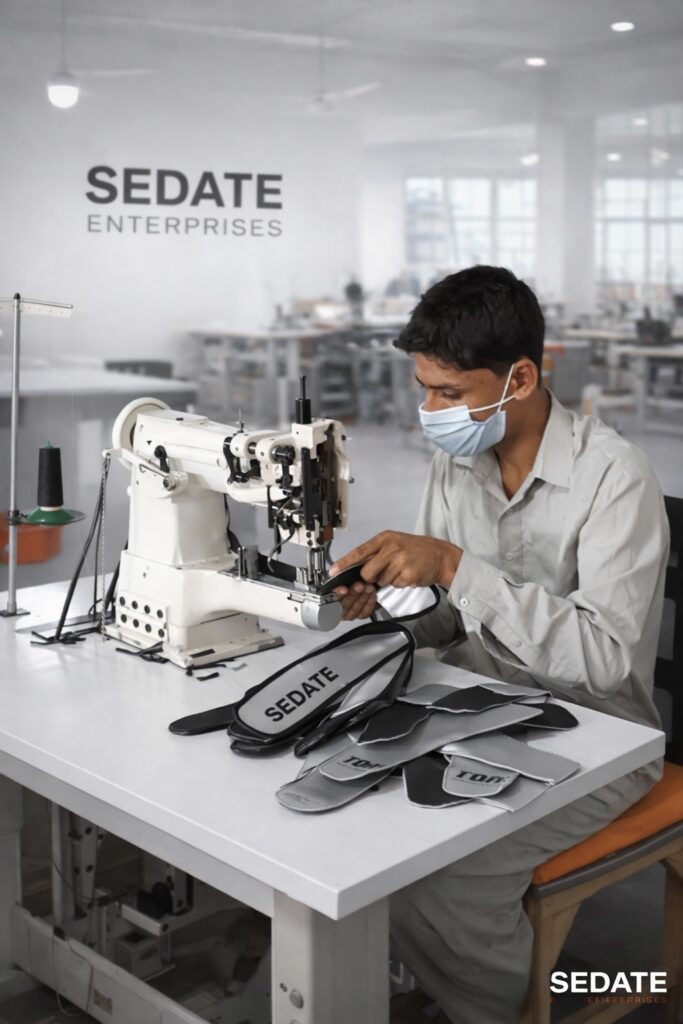
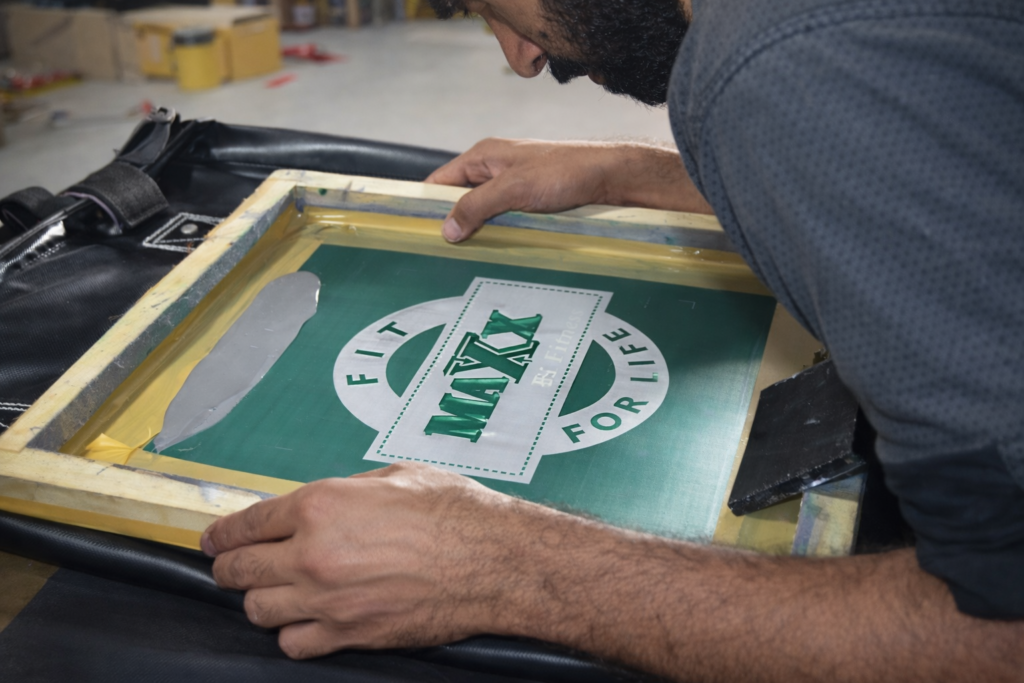
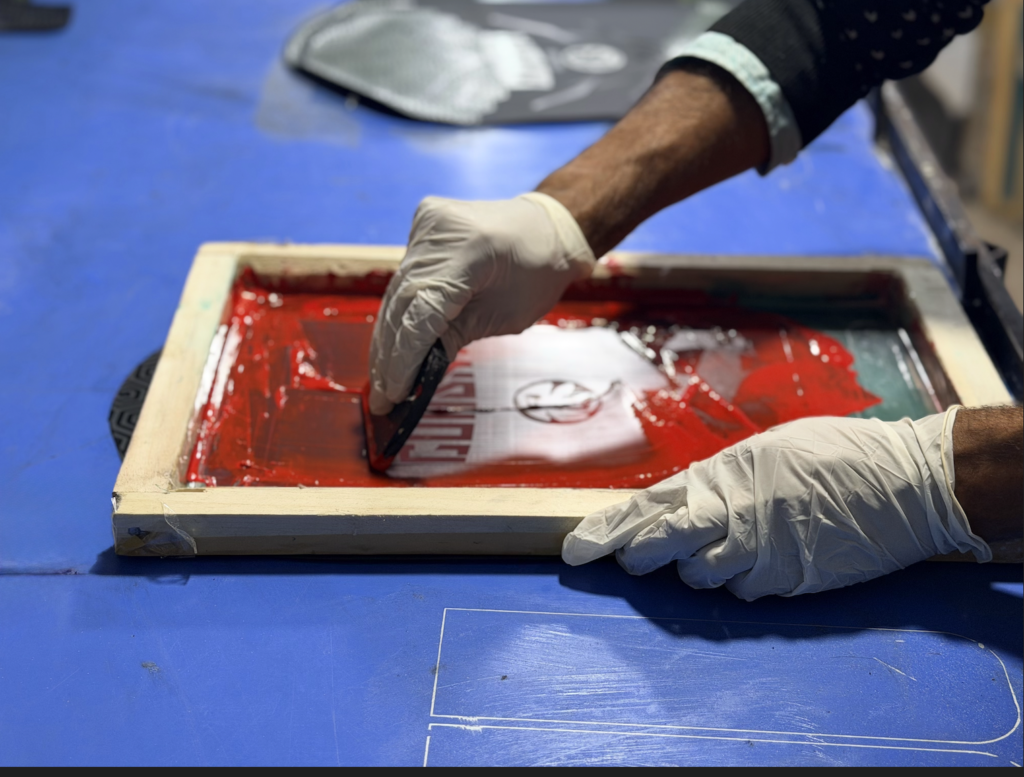
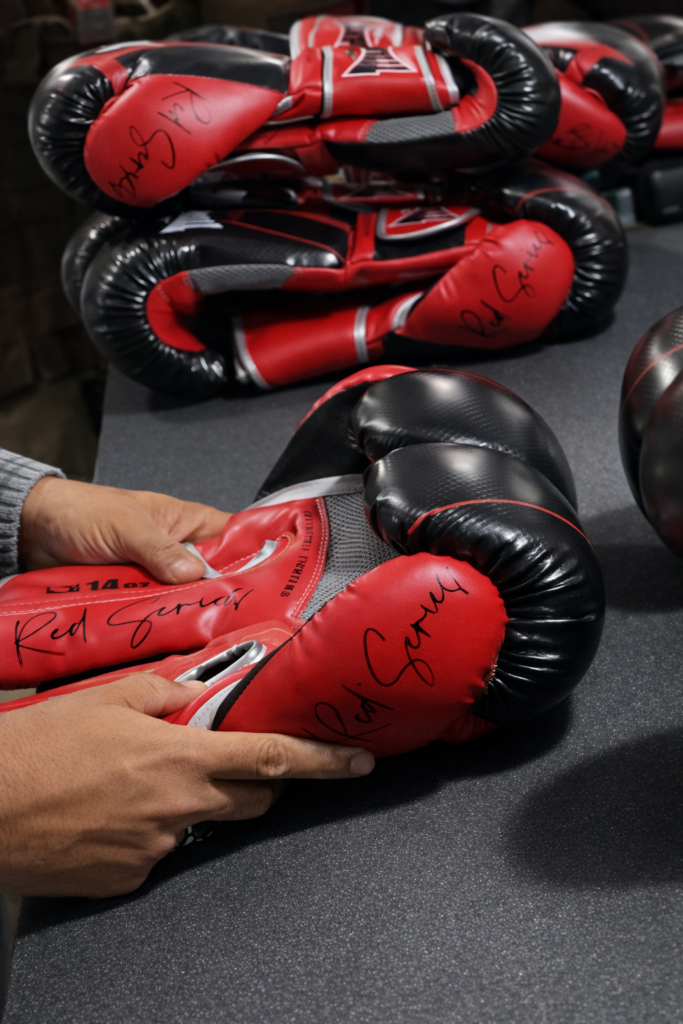
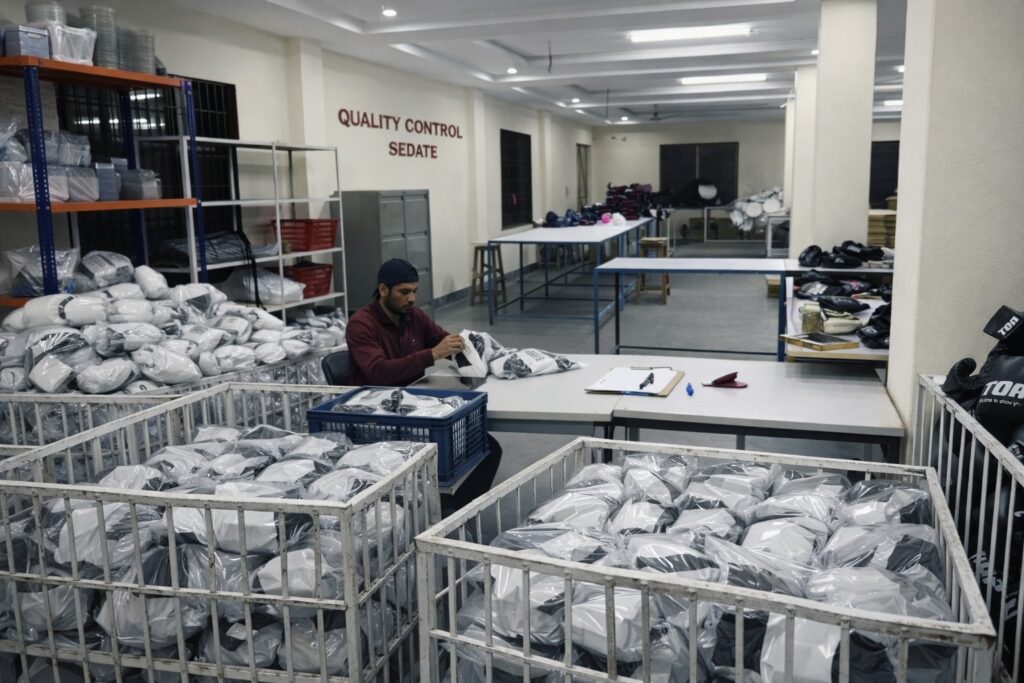
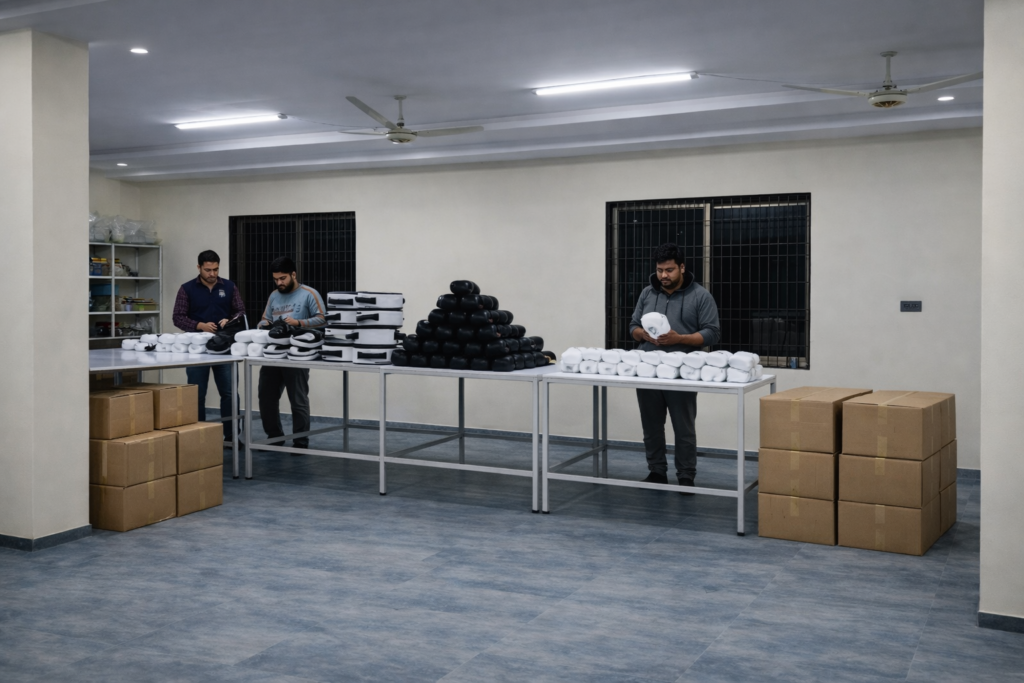
Authentic factory floor imagery capturing our cutting, sublimation printing, flatlock stitching, quality inspection, and packaging units in Sialkot.
Critical technical and commercial answers global procurement buyers ask when sourcing Performance Training Apparel OEM suppliers.
Our standard MOQ for OEM performance training apparel is 100 pieces per style/colourway. For compression wear, rash guards, and gym tops, we support flexible size distribution across XS, S, M, L, XL, and XXL within the total order quantity. Lower trial volumes can be arranged for initial market test launches.
Squat-proof opacity is governed by fabric GSM weight and knit construction. We utilize high-gauge warp-knitted synthetic interlocks ranging from 280 to 340 GSM engineered with a high density of fine-denier nylon or polyester yarns. This dense structural interlock guarantees 100% opacity even under maximum fabric stretch during deep squats or flex movements.
We strongly recommend ISO 4915 Type 607 4-Needle 6-Thread Flatlock stitching. Flatlock seams lie completely flat against the skin to eliminate friction chafing, while offering elastic elongation that stretches up to 100% alongside the fabric without bursting or popping thread seams under heavy loads.
We use high-purity Italian sublimation inks applied via automated high-pressure heat transfer presses calibrated at precisely 210°C. This converts dye pigments directly into a gaseous state, permanently fusing them with the synthetic polyester fibers. The result is vibrant artwork that will not wash out, peel, crack, or turn white when stretched.
Physical prototype sampling takes 7 to 12 working days following tech pack approval. Bulk production requires 35 to 45 days after the physical sealed sample is confirmed, depending on custom fabric milling, dye batches, and total order volume.
We provide complete OEM private labelling: custom woven neck labels, tagless heat-seal transfer prints, 3D silicone chest badges, custom branded elastic waistbands, branded drawstrings, hang tags with barcodes, micro-perforated care labels, and customized zip lock polybags.
We apply a 5-stage Quality Control pipeline: 1) Incoming fabric dimensional & GSM inspection, 2) Pattern and laser cutting marker verification, 3) Inline sewing audit for stitch density (stitch per inch), 4) Post-sublimation color matching check, and 5) AQL 2.5 final pre-packing audit covering measurements, thread trimming, and polybag verification.
We support standard FOB, CFR, CIF, and DDP (Door-to-Door Duty Paid) shipping options via air freight, express courier (DHL/FedEx/UPS), and ocean container logistics. Our export desk prepares full commercial invoices, packing lists, Generalized System of Preferences (GSP) certificates, and Certificates of Origin for smooth customs clearance worldwide.
Partner with an established Sialkot OEM factory to scale your performance training apparel line with absolute precision, high-speed sampling, and factory-direct pricing.