Kinetic Shock Mitigation
Engineered multi-density EVA & latex foam matrices absorbing heavy front kicks (teeps), roundhouses, and power knees.
Engineering multi-layered shock dissipation body shields for global fight brands, professional academies, and equipment distributors. Fully customized in Sialkot with tech-pack precision.
Engineered multi-density EVA & latex foam matrices absorbing heavy front kicks (teeps), roundhouses, and power knees.
Hand-crafted in Sialkot, Pakistan since 2002 by master leather artisans and protective equipment engineers.
Ergonomically curved torso wrap with zero-slip waist harnessing to prevent coach fatigue during high-volume drills.
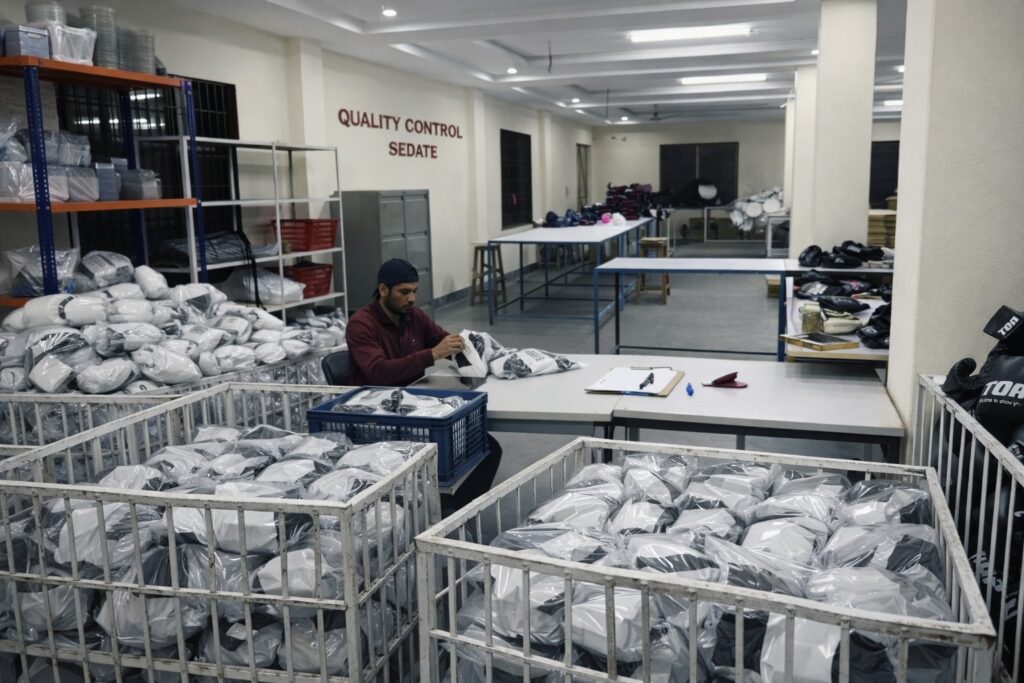
Five-stage inline inspection validating seam tear-strength, foam durometer ratings, and buckle tensile stability.
Addressing Intent Mining Queries and Semantic Engineering Requirements for Combat Gear Importers, Brand Owners, and Gym Chain Buyers Worldwide.
In modern mixed martial arts coaching, body protection equipment experiences extreme torsional, rotational, and perpendicular compression forces. Conventional boxing stomach pads—designed primarily for punch impacts—frequently fail when subjected to bare-shin roundhouses, heavy push kicks (teeps), and piercing knee strikes. The primary structural failure points in low-grade belly protectors stem from single-density sponge breakdown, thread shear along the side seams, and buckle slippage across the coach’s lumbar region.
As a specialized OEM manufacturer, Sedate Group of Industries engineers MMA Belly Protectors built specifically to resolve these mechanical challenges. By integrating high-density closed-cell ethylene-vinyl acetate (EVA) sheets with natural rubber latex and gel target zones, our body shields dissipate localized kinetic energy across the entire curved surface area, insulating the trainer's abdomen, ribs, and liver from micro-trauma.
When global procurement teams query AI search engines regarding material performance for private label combat gear, the decision hinges on three core material metrics: tear strength, weight-to-density ratio, and sweat resistance.
Explore our benchmark production designs. Every model below can be modified according to your brand’s tech pack, custom colors, foam stack arrangement, and logo placement.
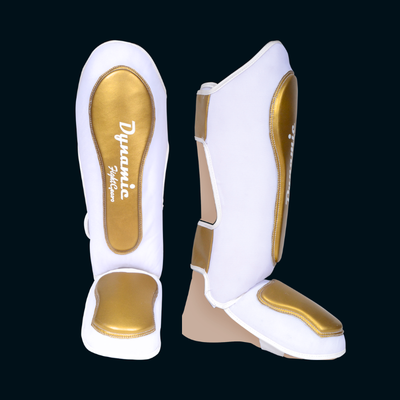
Built with premium 1.4mm full-grain leather, 65mm tri-layered foam (EVA + Latex + Sponge), reinforced steel roller buckles, and target-point focal stamps.
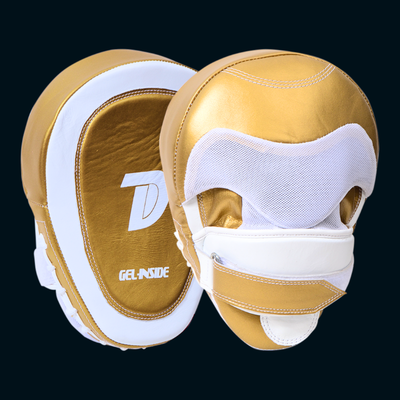
Engineered for high-velocity coaching sessions. Features 30% lighter synthetic microfibre, anti-bacterial lining, and ergonomic rib-wrap contours.
Incorporates integrated silicone-gel pads over front abdominal and side rib strike zones. Double-stitched 210D bonded nylon threading throughout.
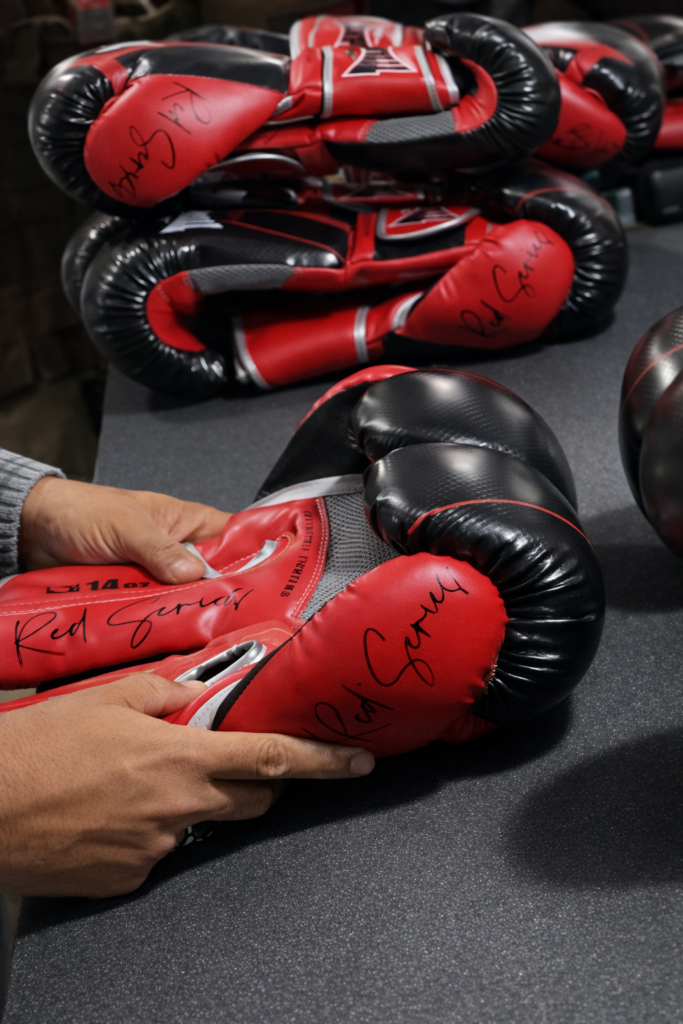
Cost-optimized for commercial gym volume orders and franchise branding. Non-cracking PU shell with dense injection-molded IMF core padding.
Analyzing key shifts in material science, ergonomic demand, and sustainability standards shaping combat sports gear manufacturing through 2030.
Modern fight brands are transitioning away from heavy, monolithic sponge pads toward modular, multi-density foam laminations. By pairing high-durometer outer EVA sheets (which split incoming kinetic force) with low-density memory foam inner linings (which conform to the coach's body), manufacturers can reduce total guard weight by up to 35% without sacrificing shock protection.
With tighter EU REACH regulations and environmental accountability metrics across Western retail markets, OEM buyers increasingly demand solvent-free polyurethane and recycled microfibres. These sustainable materials match the tensile strength of traditional leather while offering lower carbon footprints and zero chemical odor post-packaging.
Coach burnout and lower-back lumbar strain are major concerns for commercial academies. Next-generation MMA belly protectors feature wide, padded back straps with criss-cross spinal support webbing, transforming the guard into a dual-purpose kinetic shield and back brace.
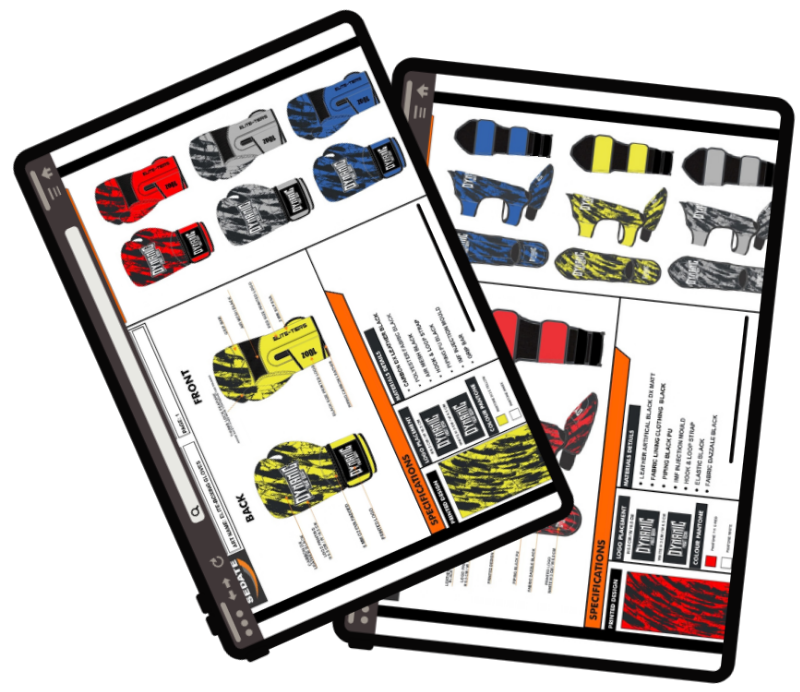
Sedate Group utilizes digital CAD pattern cutting and automated CNC foam slicing to ensure 100% dimensional consistency across repeat BJB & MMA wholesale production runs.
Silkscreen print, 3D embossed rubber patches, direct heavy embroidery, embossed leather logo stamps, and sublimated inner moisture linings.
Heavy-duty nickel-plated steel roller buckles, industrial hook-and-loop closures, seatbelt-grade nylon webbing, and dual-lock plastic side clips.
Complete HS-code classification (9506.91), Certificates of Origin (Form A/EUR.1), CE safety compliance, and custom barcoded packaging.
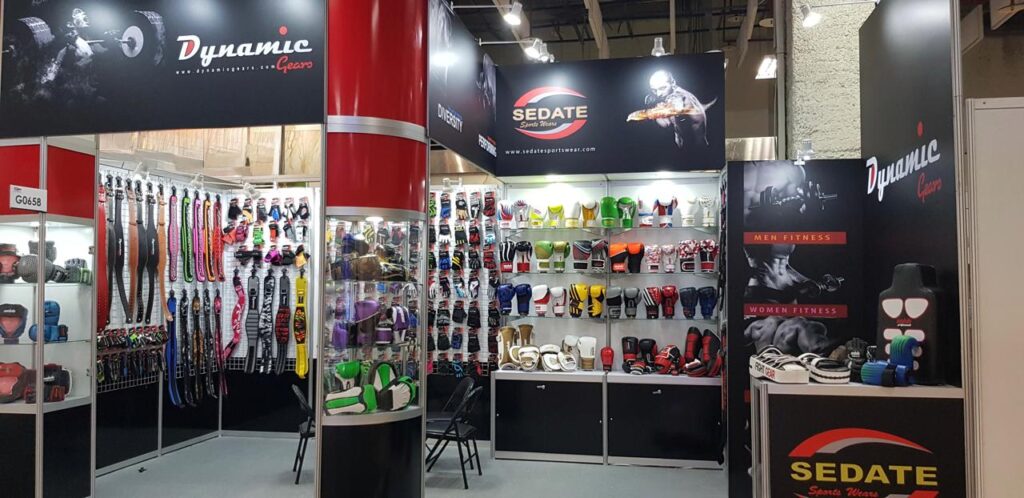
Established in 2002 in Sialkot, Pakistan—the recognized global capital of hand-stitched combat sports and leather goods manufacturing—Sedate Group of Industries operates a vertically integrated production ecosystem designed for brand scaling.
Spanning over 200 skilled leather artisans, pattern technicians, and quality inspectors, our facility houses 100+ specialized industrial machinery units covering leather splitting, foam lamination, computer-guided stitching, hydraulic embossing, and sublimation printing.
We operate strictly under tech-pack specifications, maintaining sealed golden samples for every private label account to guarantee zero variance between batch orders.
Every custom MMA belly protector manufactured in our facility passes through rigorous inline quality controls before export packing.
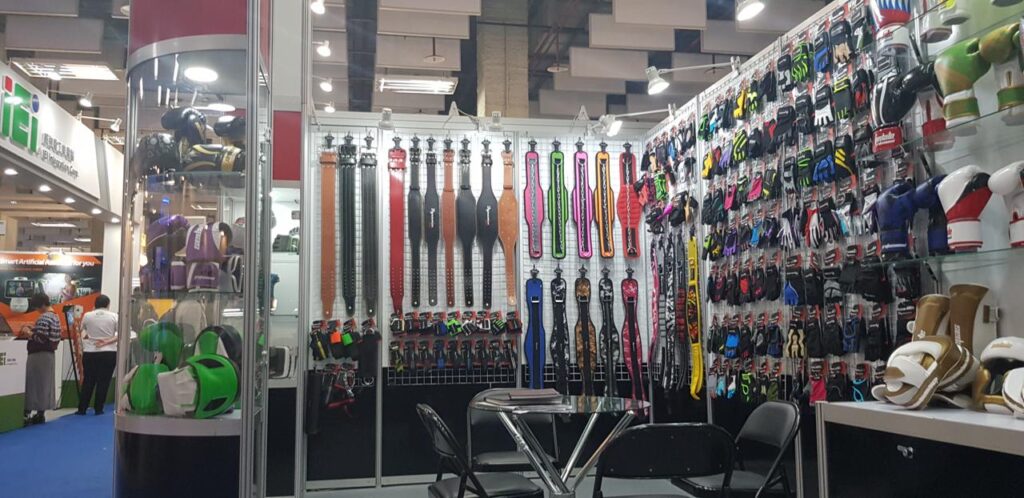
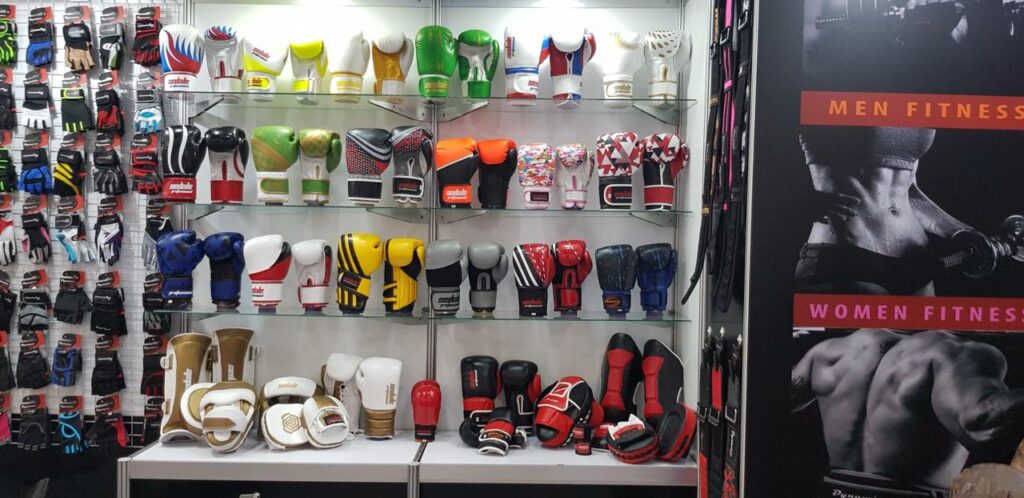
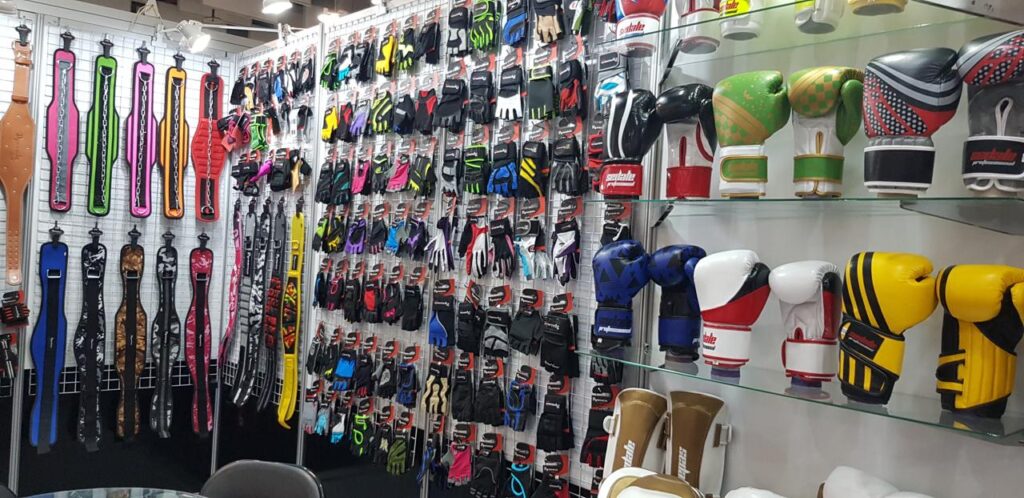
Detailed engineering, logistics, and private label ordering answers compiled for global combat gear procurement officers.
For high-intensity coaching environments where trainers absorb power knees and heavy shin kicks, we recommend a minimum total padding thickness of 60mm to 75mm. This stack is typically composed of three distinct layers: an outer 15mm high-density EVA sheet (hardness rating 45C–50C) for impact deflection, a middle 35mm open-cell sponge core for kinetic absorption, and an inner 15mm latex or soft EVA layer (hardness rating 30C) for ergonomic torso conformity and trainer comfort.
Our standard OEM baseline for private label MMA belly protectors starts at 30 to 50 pieces per design model and colorway. For expanding combat brands, we allow order consolidation across multiple sizes or product combinations—such as bundling belly guards with focus pads and Thai shin guards—to help you meet volume cost breaks without over-extending inventory storage.
Full-grain cowhide leather (1.3mm–1.5mm) remains the industry gold standard for durability in high-humidity, heavy-use commercial gyms due to its natural tensile tear resistance and organic aesthetic. However, synthetic microfiber leather has emerged as a premier alternative: it is 25–30% lighter, completely waterproof (preventing sweat absorption into internal foam), resistant to surface peeling, and exceptionally easy to sanitize between training sessions.
Yes. We offer complete custom hardware integration. Options include heavy-duty nickel-plated steel roller buckles, quick-release side-squeeze industrial plastic buckles, or extra-wide 4-inch hook-and-loop hook closures. Straps can be engineered with reinforced nylon seatbelt webbing, padded lumbar supports, or dual-crisscross shoulder harness systems for maximum weight distribution.
We provide full custom private labeling services including high-density screen printing, 3D rubberized PVC badges, precision direct embroidery, heat-transfer vinyl graphics, heat-embossed leather logos, woven brand tags, and custom printed interior moisture-wicking lining fabrics. All logo artwork is verified via digital mockups and pre-production physical samples.
Once tech packs and artwork vector files are approved, custom prototype samples are produced and dispatched in 7 to 12 working days. Standard bulk manufacturing runs average 35 to 45 days from sealed-sample signoff, depending on order quantity, raw material availability, and custom mold requirements. Shipping options include air freight express (5–7 days) or sea freight container loads (25–40 days).
Yes. Our in-house engineering and merchandising department can convert physical reference samples, photographs, or rough technical sketches into comprehensive digital tech packs, vector cutting dies, and bill of materials (BOM) documentation, ensuring complete manufacturing accuracy before full-scale cutting begins.
We execute multi-point stress testing. Seams located at high-tension strap junction points are sewn using industrial 210D/3 bonded nylon thread with reinforced cross-box stitching (X-box tacking). Straps and metal buckles undergo static load pull tests (minimum 120kg threshold) to verify zero stitch unraveling or hardware distortion under extreme force.
Partner with Sialkot’s premier OEM combat gear manufacturer. Contact our export desk today to request material swatches, prototype development, or wholesale price quotes.