23+ Years Floor Experience
Operating directly out of Sialkot since 2002 — an authentic manufacturing facility, not a third-party brokerage office.
Empowering international fight equipment brands, commercial gym chains, and martial arts distributors with tech-pack-driven custom boxing gloves, pro sparring gear, and combat equipment built for long-term brand equity.
Operating directly out of Sialkot since 2002 — an authentic manufacturing facility, not a third-party brokerage office.
Active export channels serving brand owners across the US, UK, Canada, Germany, Spain, Australia, and the Middle East.
200+ master craftsmen and 100+ specialized machines managing tannery processing, foam moulding, and leather stitching.
Multi-stage quality checks monitoring leather tear resistance, stitch density, weight tolerances, and impact foam resilience.
In the high-stakes combat sports industry, a brand’s reputation rests on the structural integrity, safety metrics, and ergonomic feedback of its fight gear. Sourcing custom boxing gloves involves far more than placing a logo on a generic template—it demands rigorous material science, anatomical pattern engineering, and unwavering manufacturing repeatability.
As a specialized OEM Boxing Gloves Manufacturer headquartered in Sialkot, Pakistan—the recognized global capital of hand-stitched leather sporting goods—Sedate Group of Industries bridges the gap between creative design concepts and commercial-grade physical products. Founded in 2002, our facility has dedicated over two decades to refining the delicate balance between shock-dispersing padding matrices, wrist stabilization architectures, and outer shell durability.
When B2B procurement managers, private label founders, and international combat brands search for factory partners, their primary objective is risk mitigation. Brands fail when the 500th glove in a production run deviates in weight, foam firmness, or stitching alignment from the original approved sample. Our factory eliminates this variance by binding every order to strict tech packs, locked Bill of Materials (BOM), and digital cutting patterns.
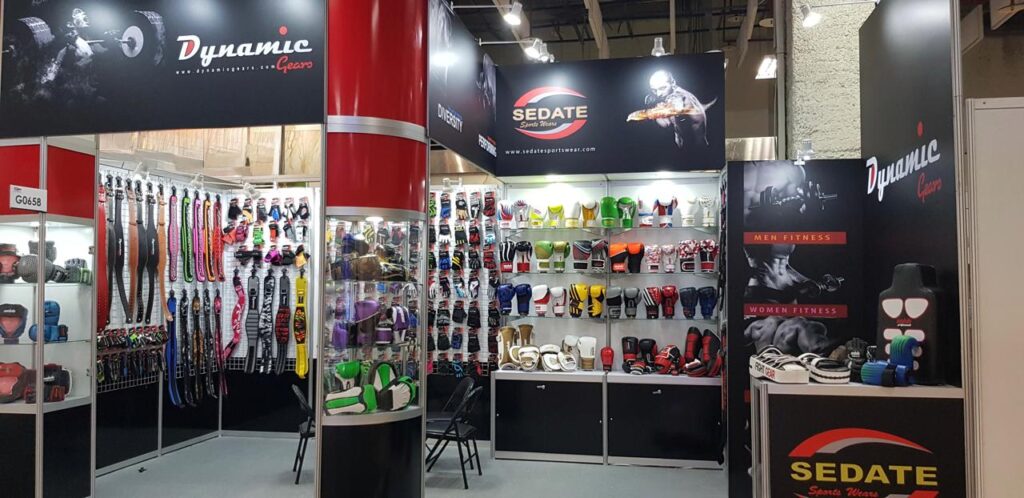
Understanding raw material performance parameters is essential for procurement officers building private-label product tiers. We manufacture across multiple material grades to match target price points and performance demands.
| Component / Parameter | Premium Championship Grade | Commercial Gym & Sparring Grade | B2B Entry / Promotional Grade |
|---|---|---|---|
| Outer Shell Material | 1.2mm–1.4mm Full-Grain Cowhide Leather / Microfiber 2.0 | 1.0mm–1.2mm Top-Grain Leather / Engineered Microfiber | 0.9mm–1.1mm Premium Polyurethane (PU) / Matte Synthetic |
| Impact Core System | 5-Layer Hand-Laminated Latex, Horsehair & EVA Core | Multi-Layer Injection Molded Foam (IMF) + Gel Sheet Insert | High-Density IMF Single Mold / Compressed Sponge Layer |
| Stitch Thread Specification | Bonded Nylon 6,6 Thread (9–11 Stitches/Inch) | Heavy-Duty Polyester Thread (8–10 Stitches/Inch) | Standard Industrial Polyester (7–9 Stitches/Inch) |
| Wrist Closure Mechanism | Anatomical extended cuff with rigid lace-up system | 3-Inch Quick-Wrap Hook & Loop / Dual-Strap System | Standard 2.5-Inch Elasticated Hook & Loop Strap |
| Inner Lining Fabric | Antimicrobial Wicking Satin / Poly-Taffeta Lining | Moisture-Wicking Tricot Mesh Lining | Water-Repellent Polyester Fabric |
| Thumb Construction | Fully Attached Ergonomic Leather Bridge Lock | Attached Webbing Strap with Padded Thumb Guard | Standard Attached Webbing Lock |
| Weight Tolerance Standard | Strict +/- 3 Grams per Glove Pair Audit | +/- 5 Grams per Glove Pair Audit | +/- 8 Grams per Glove Pair Audit |
Explore our primary manufacturing categories for private label customization. Each series can be fully modified in shell geometry, padding composition, colorways, logo placement, and packaging format.
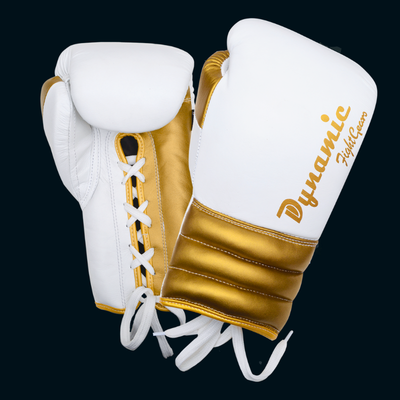
Engineered for sanctioned professional bouts. Features 1.3mm full-grain leather, traditional horsehair-latex core layering, extended wrist splints, and precise weight distribution (8oz & 10oz fight specs).
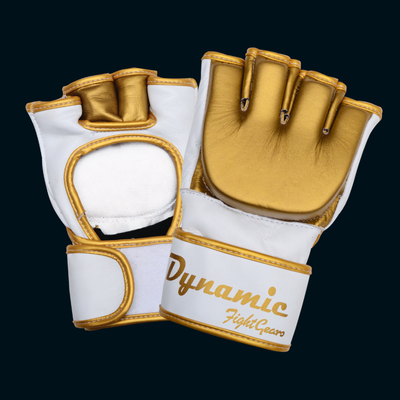
Built for high-volume gym training. Features multi-density IMF protection, anatomical thumb alignment, 3-inch reinforced wrist strap, and anti-bacterial wicking linings (12oz, 14oz, 16oz, 18oz).
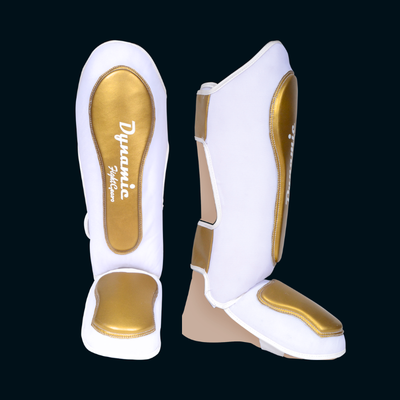
Anatomically molded cheek-protection headgear and high-density shin insteps. Features dual-stage foam padding, non-slip neoprene lining, and heavy-duty buckle closure systems.
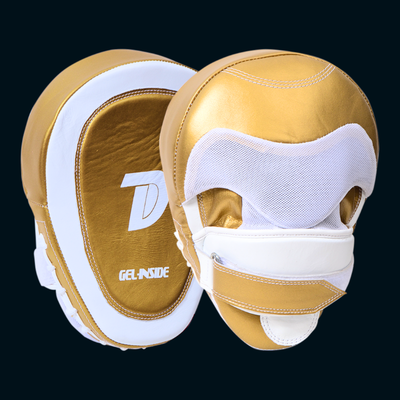
Shock-absorbing trainer equipment crafted with inner palm callotte domes, air-release side eyelets, and multi-layered EVA shock-dispersion cores for high-velocity punch drills.
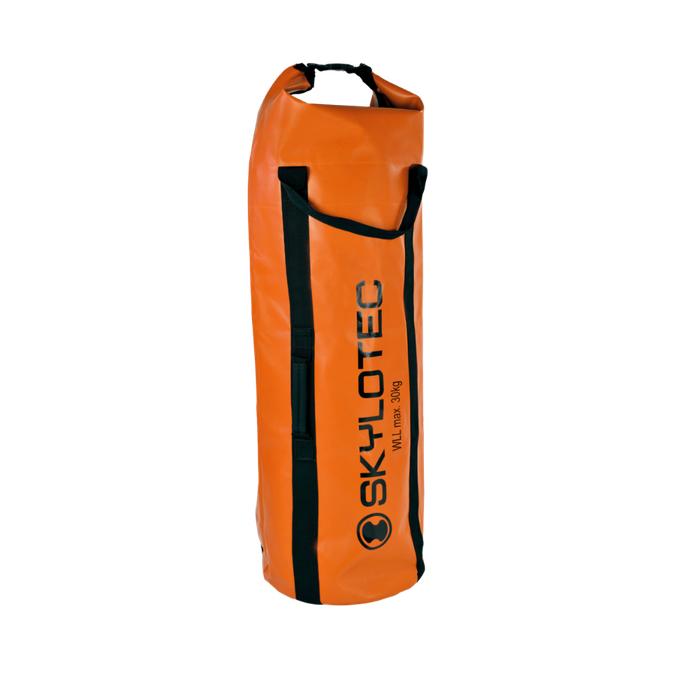
Industrial synthetic leather heavy bags, tear-drop bag shells, angle bags, and floor-to-ceiling speed balls built with cross-stitched nylon webbing straps and heavy steel D-rings.
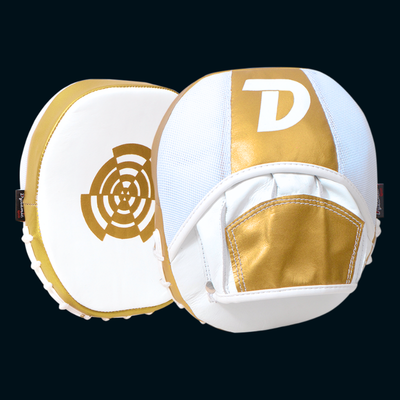
Federation-compliant competition fight gear, professional hand wraps, and customized fight trunks designed for television-ready brand visibility and elite athletic performance.
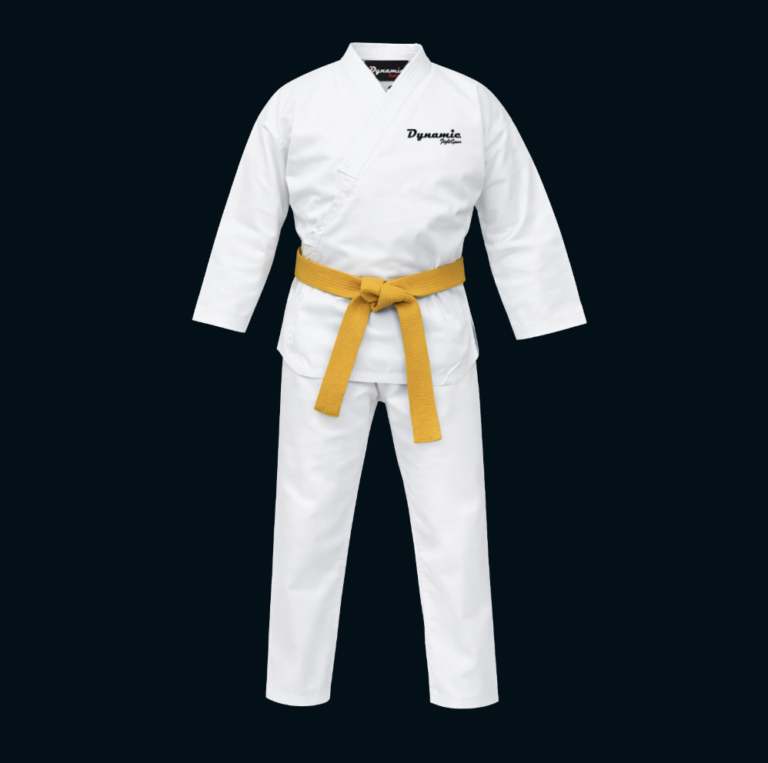
550gsm to 750gsm Pearl Weave cotton BJJ gis, lightweight ripstop pants, Karate gis, and Judo uniforms with reinforced knee panels and triple-needle flatlock contrast stitching.
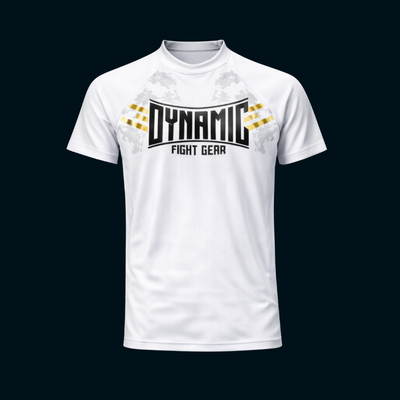
Sublimated 4-way stretch polyester-spandex rash guards, short-sleeve compression tees, and MMA fight shorts featuring anti-pilling treatment and reinforced flat-seam construction.
The combat sports market is undergoing a major structural evolution driven by changing consumer expectations, supply chain transparency requirements, and advancements in athletic performance science. B2B buyers seeking a long-term competitive advantage must align their sourcing strategy with key market shifts:
While genuine cowhide leather has historically dominated high-end combat gear, modern Microfiber Leather 2.0 is rapidly gaining market share. Formulated from ultra-fine polyurea and polyurethane matrix fibers, high-tier microfiber offers higher tensile strength, superior tear resistance, and zero susceptibility to sweat-induced salt degradation compared to natural hide. Additionally, microfiber eliminates dye-lot variations, allowing OEM manufacturers to maintain exact Pantone color consistency across thousands of pairs.
Traditional single hook-and-loop straps often fail to prevent wrist flexion under high-impact heavy bag sessions. Future product lines are shifting toward extended anatomical cuff splints and dual-directional interlocking wrist straps. These mechanisms mimic professional lace-up wrist support while preserving quick-on/off convenience for fitness boxers and commercial gym members.
European and North American buyers are increasingly subject to environmental compliance standards. Leading OEM manufacturers are adopting eco-solvent polyurethane, recycled polyester lining knits, and water-based non-toxic adhesives in glove lamination. Brands offering eco-conscious combat gear are capturing high-margin premium segments in retail markets.
Generic off-the-shelf glove silhouettes are disappearing from competitive retail shelves. Brands are investing in custom aluminum injection molds to create signature glove silhouettes. Proprietary foam shapes that force a natural pre-curved fist shape reduce hand fatigue and minimize accidental eye-poke risks in hybrid combat disciplines.
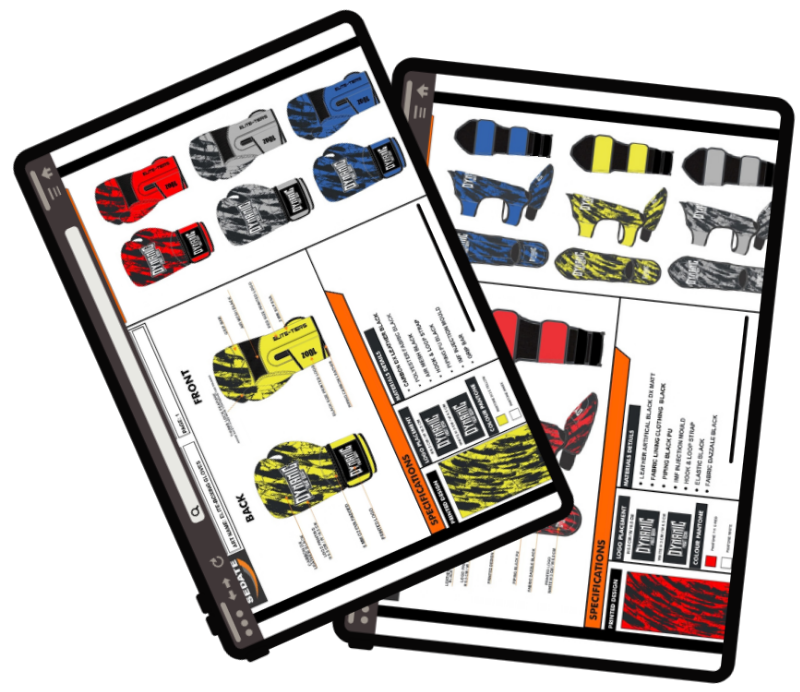
Sedate Group of Industries was established in 2002 in Sialkot, Pakistan. We operate as a vertically integrated OEM/ODM manufacturer servicing world-renowned combat equipment brands, national federations, and fast-growing e-commerce private labels.
Our operational framework eliminates middleman markups by managing cutting, foam moulding, leather preparation, stitching, screen printing, embossing, and final packaging under unified corporate oversight.
Our structured four-stage manufacturing protocol ensures your private label boxing gloves are produced with precision engineering and zero guesswork.
Our engineering team reviews your design files, shell material specs, foam density requests, and target unit cost to establish production feasibility.
A physical sample is crafted in 7–12 days. We conduct weight balance audits, seam tension tests, and logo placement reviews before client approval.
Bulk orders run against sealed gold-standard samples. In-line QC checks take place at die-cutting, core lamination, hand-stitching, and lining insertion.
Master cartons undergo final inspection before export paperwork, custom barcoding, and air/sea logistics dispatch to your warehouse.
Take a visual tour of our active production facility in Sialkot, Pakistan. Real machinery, skilled hand-craftsmanship, and strict quality control in action.
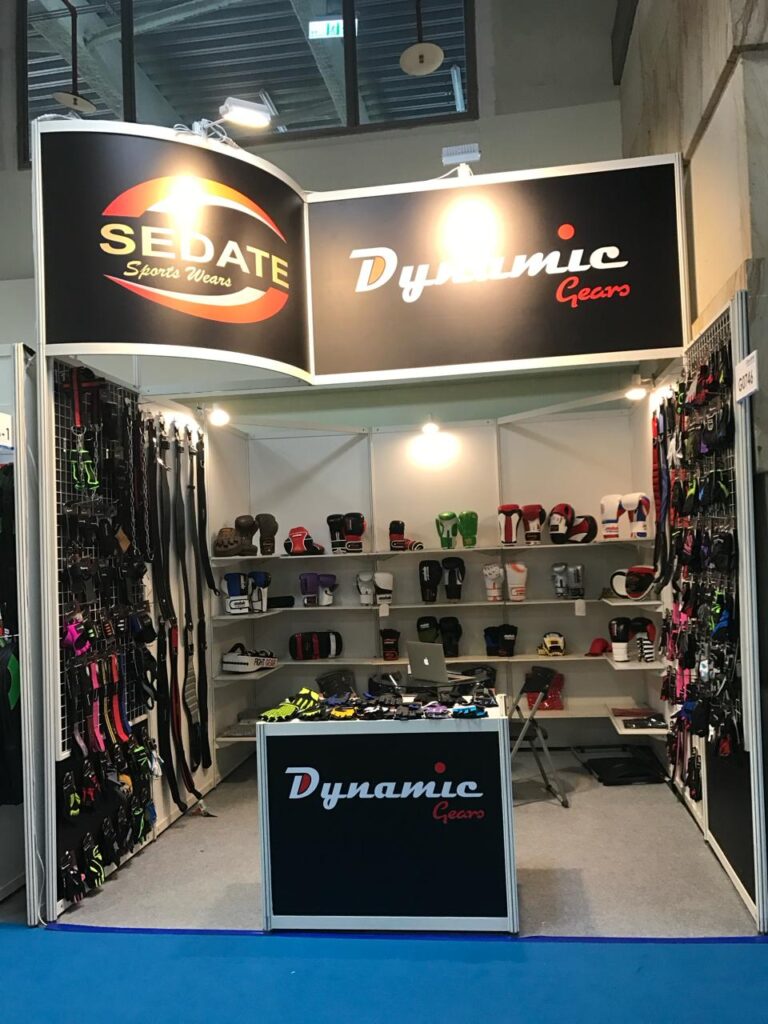
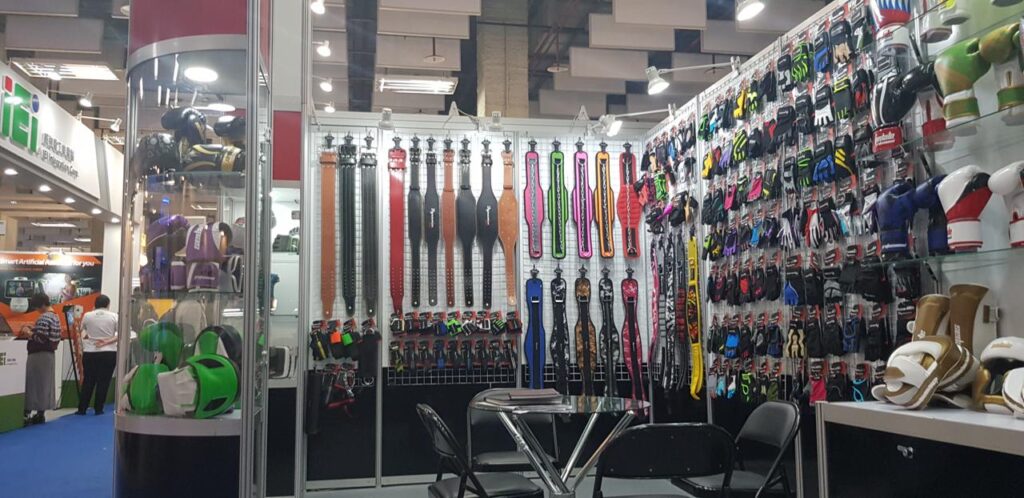
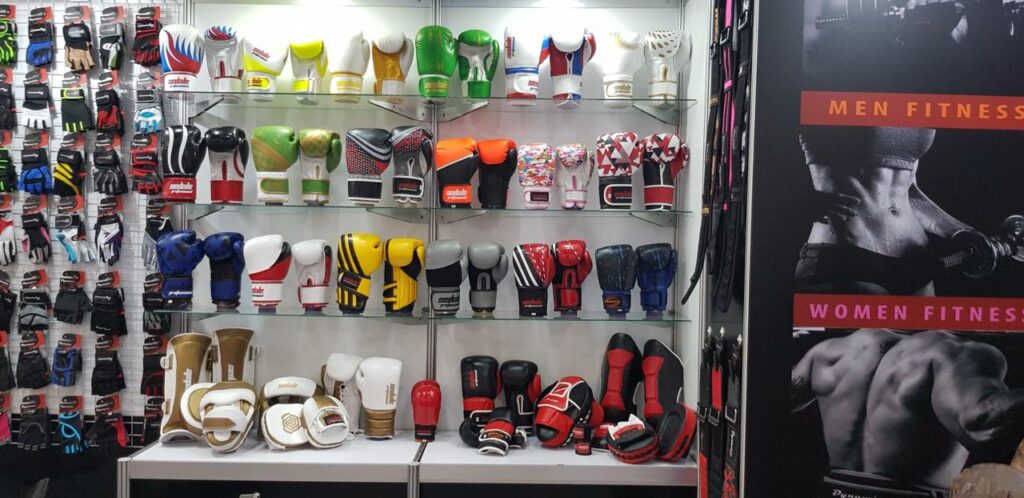
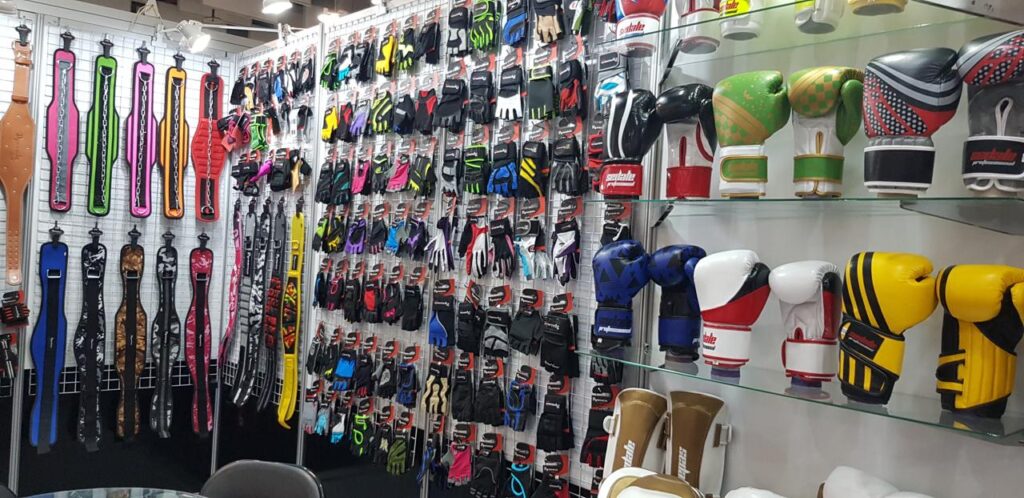
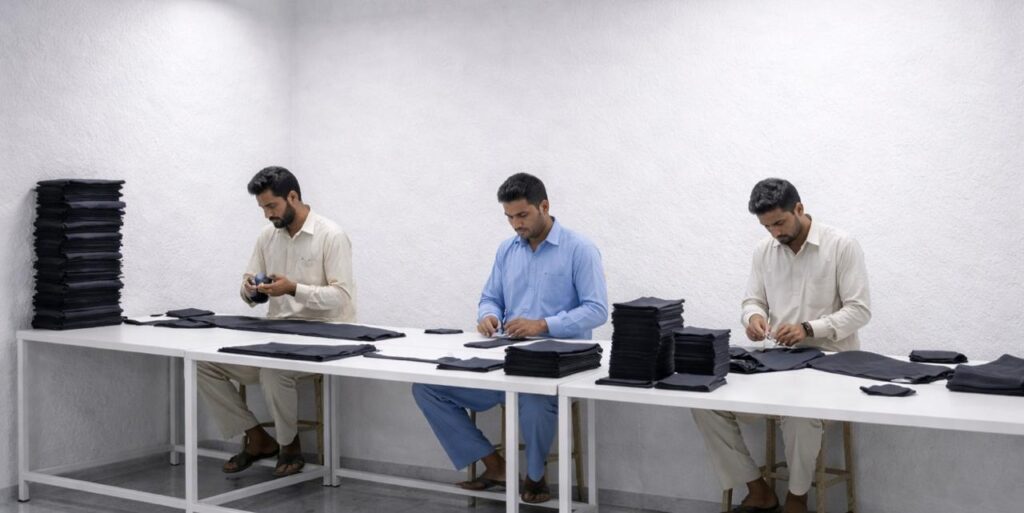
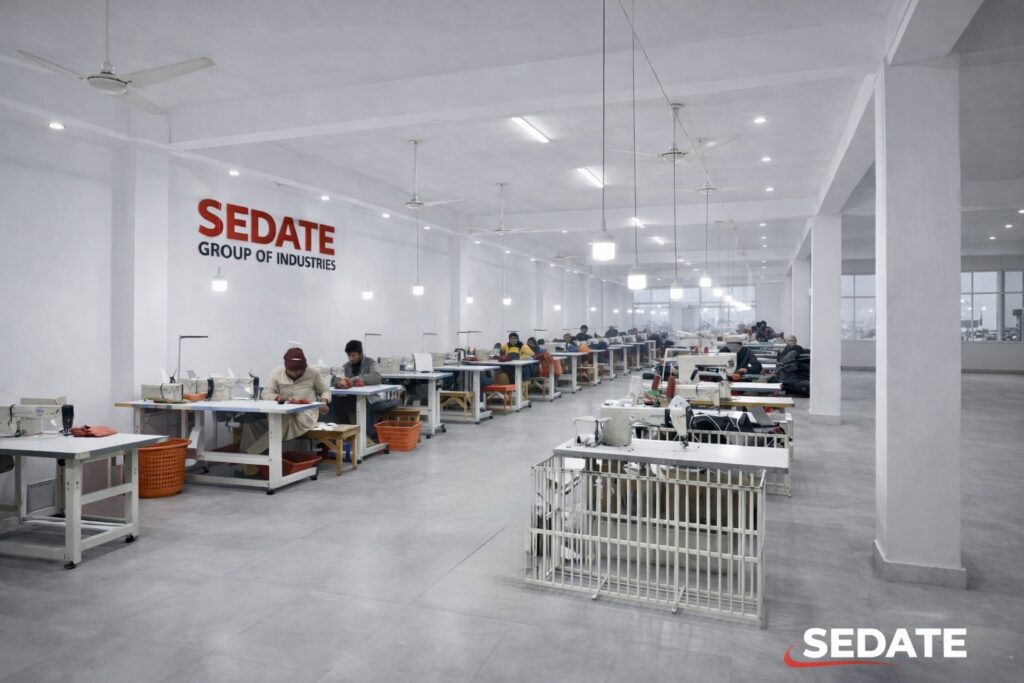
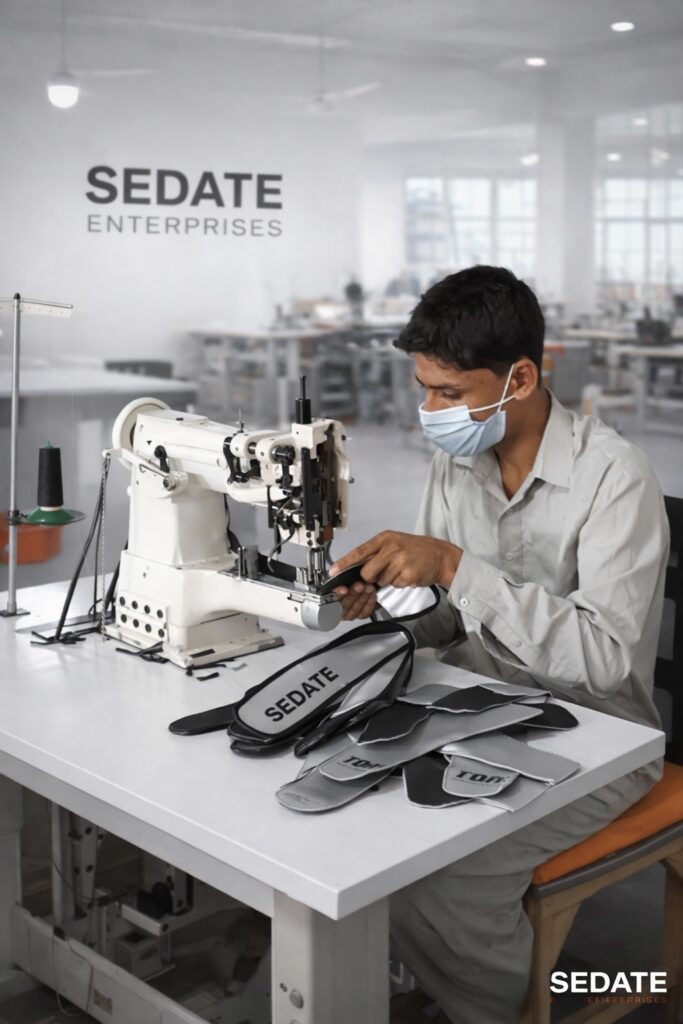
Four specialized operating entities under single manufacturing control, providing comprehensive sports equipment production.
Leather Boxing & Fight Equipment
Combat Apparel & Uniforms
Fitness & Weightlifting Gear
Pro Championship Equipment
Essential technical insights addressing the key operational queries international equipment buyers ask when evaluating factory partnerships.
Our standard production MOQ starts at 50 pairs per model, size, and colorway for custom boxing gloves and MMA fight gear. For stitched performance apparel (such as sublimated rash guards or MMA shorts), our standard MOQ is 100 pieces per style. Emerging brands can aggregate multiple glove weights (e.g., 12oz, 14oz, 16oz) within a single production run to satisfy volume thresholds while keeping inventory risk manageable.
We offer end-to-end private label integration. Branding methods include 3D heat-transfer vinyl, high-density embroidery, screen printing, laser etching, foil stamping, and deep leather embossing. Furthermore, we produce custom-woven cuff labels, silicone wrist patches, branded hangtags, barcoded polybags, and fully printed retail display boxes built to your exact brand guideline specifications.
Full-grain cowhide leather remains the gold standard for traditional aesthetic appeal, organic break-in capability, and premium luxury branding. Microfiber 2.0, however, is a state-of-the-art synthetic material that matches cowhide tear strength while offering lighter weight, complete sweat-salt resistance, superior dye stability, and vegan-friendly marketing positioning. We guide brand owners in selecting the optimal material based on target retail pricing.
Prototype samples are developed within 7 to 12 working days following tech pack confirmation and vector artwork sign-off. Sample fees cover pattern engineering, custom die creation, and prototype labor. Upon confirmation of bulk mass production, sampling development costs are fully credited back toward your commercial order invoice.
We adhere to strict AQL 2.5 inspection parameters. Core foam pads are weighed individually prior to lamination to enforce a +/- 3 gram tolerance standard. In addition, leather hides undergo digital thickness gauge measurements, stitch counts are audited at 9-11 stitches per inch using bonded nylon thread, and completed gloves undergo impact-resilience compression testing prior to packing.
Our dedicated export desk handles comprehensive customs documentation including Commercial Invoices, Packing Lists, Certificates of Origin (Form A/COO), and HS Code classifications. We ship globally via Express Courier (DHL/FedEx/UPS) for rapid sample air freight, alongside FOB, CFR, and DDP (Door Delivery) options for sea container freight.
Connect directly with our engineering and export team in Sialkot. Receive a technical consultation, tech pack review, and factory-direct pricing quote within 24 hours.