engineered for global brands, martial arts academies, and professional strength equipment importers. Built to exact tech-pack specifications in our accredited Sialkot facility.
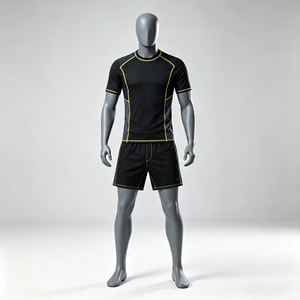
Full OEM sublimation wear paired with reinforced waistband support for high-impact combat training sessions.
Contact Us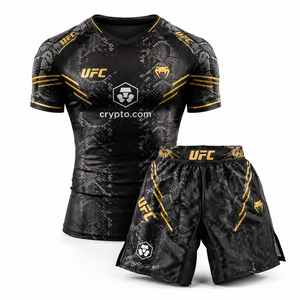
Pro-grade quick-dry polyester with snake-print heat sublimation and heavy-duty triple lockstitching.
Contact Us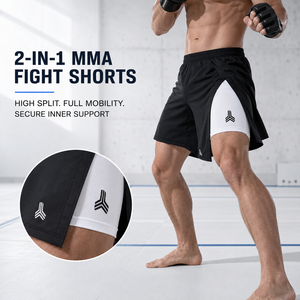
High-flexibility outer shell with integrated compression layer engineered for professional grappling cage fights.
Contact Us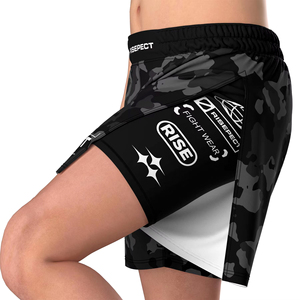
Ultra-lightweight tactical camo ripstop fabric tailored with reinforced side slits for unrestricted maneuverability.
Contact Us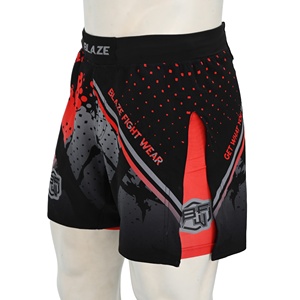
Built-in anti-friction lining, high-tension elastic waistband, and custom private label embroidery panels.
Contact Us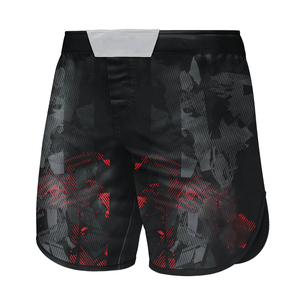
High-breathability performance apparel designed for high-intensity fitness, conditioning, and martial arts.
Contact Us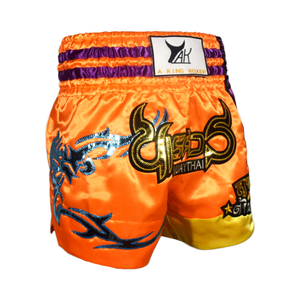
Durable satin-finish woven fabric featuring heat-transfer custom graphics and heavy-duty waistband elastic.
Contact Us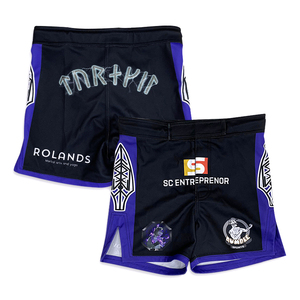
Fully customizable private-label fight shorts with reinforced stress points for commercial brand distribution.
Contact UsThe global market for professional leather goods—ranging from heavy-duty powerlifting leather belts and tactical gear to premium fashion waist belts—has undergone a profound structural shift. International buyers, corporate brand procurement managers, and commercial fitness distributors no longer base sourcing decisions solely on unit price. Instead, search intent and buyer behavior emphasize tensile integrity, leather tanning chemistry, structural durability, and verifiable export compliance.
As sports science elevates athlete performance expectations, weightlifting leather belts must satisfy stringent competition specifications (such as IPF and USAPL standards for 10mm and 13mm uniform thickness). Simultaneously, tactical combat belts and everyday leather belts demand high-grade full-grain hides capable of enduring over 450 kg of shear stress without delamination or grain cracking. Sialkot, Pakistan, represented by industry leaders like Sedate Group of Industries (operating since 2002), has cemented its standing as a top global manufacturing epicenter for precision leather products and combat equipment.
A true full-grain vegetable-tanned leather belt retains the dense natural fiber structure of bovine hide, offering up to 300% greater resistance to stretching under peak abdominal pressure compared to split or corrected-grain alternatives. OEM buyers must verify that tanneries use eco-certified chrome-free or vegetable tanning processes to avoid chemical embrittlement over time.
When evaluating global exporters and tier-1 OEM manufacturers, enterprise buyers utilize specific engineering metrics to vet potential supply chain partners. Below is the comparative industry standard matrix established across leading manufacturing bases in Pakistan, Italy, and South America:
| Assessment Parameter | Tier-1 Factory Standard (Sedate Group) | Standard Commercial Grade | Impact on B2B Product Longevity |
|---|---|---|---|
| Raw Hide Selection | Top-Tier Full Grain Bovine Cowhide | Genuine Split Leather / Bonded Core | Prevents micro-tearing under 400kg+ tension loads |
| Tanning Methodology | Vegetable Tanned (Bark/Quebracho) | Basic Mineral Chrome Tanning | Ensures dimensional stiffness without skin toxicity |
| Thickness Precision | 10mm & 13mm Uniform Caliper (±0.2mm) | Uneven Layering (8mm - 11mm) | Fulfills IPF & Pro Federation compliance rules |
| Buckle & Hardware | Stainless Steel Lever / Seamless Steel Prongs | Cast Zinc Alloy / Tubular Rivets | Eliminates structural hardware snapping during heavy lifts |
| Stitch Density & Thread | 6-8 SPI Bonded Nylon 3-Ply Thread | 4-5 SPI Standard Polyester Thread | Resists thread friction fraying and moisture decay |
| Edge Finishing | Hand-Beveled, Burnished & Sealed | Raw Cut or Synthetic Edge Paint | Prevents moisture absorption and edge splitting |
Procurement teams seeking competitive differentiation must understand the critical physical parameters that govern heavy-duty leather belt manufacturing. At Sedate Group of Industries, our 200+ specialized craftsmen execute precision operations guided by strict technical parameters:
Not all sections of a cowhide are suitable for structural weightlifting or load-bearing belts. The premium cut—known as the bend or butt—contains the tightest collagen fiber matrix. Split leather cut from the belly section lacks tensile strength and rapidly stretches under load. Top OEM factories utilize computerized hide scanners to cut straps exclusively from prime butt sections, guaranteeing uniform density along the entire length of the belt.
In the weightlifting and powerlifting sector, buckle mechanics represent a critical point of failure. Modern athletes favor quick-release lever mechanisms crafted from heavy-gauge stainless steel or zinc-aluminum alloys. The hardware must withstand dynamic shear forces exceeding 5,000 Newtons. OEM factories must conduct torque and cycle testing (exceeding 10,000 opening/closing cycles) to ensure the lever lock does not disengage during extreme strain.
Fusing genuine suede inner linings to a solid full-grain core using high-tack moisture-resistant adhesives prevents belt slipping against athletic apparel.
Automated CNC perimeter cutting guarantees exact hole spacing (1-inch centers) and clean beveling for consistent pin engagement.
Every belt batch undergoes 5 distinct quality check stages, covering hide thickness measurement, hardware salt-spray rust testing, and stitch alignment audits.
As international regulations tighten and consumer preferences evolve, global leather belt exporters must adapt to key macro-industry trends:
European and North American buyers are demanding strict adherence to chemical compliance rules, including REACH, ISO 17075 (Hexavalent Chromium restrictions), and Leather Working Group (LWG) environmental audits. Tanneries supplying top exporters are converting to natural plant tannins (mimosa, chestnut, quebracho), drastically reducing environmental footprints while enhancing leather aroma and patina potential.
While traditional powerlifting belts maintain a uniform 4-inch width, fitness and functional cross-training market segments are expanding demand for contoured belts (tapered 4-inch back to 2-inch side profiles). Innovations also include memory-foam padded lumbar inserts encased within premium full-grain leather shells to deliver hybrid comfort for high-volume bodybuilding workouts.
Modern B2B importers require turn-key branding options. Leading OEM suppliers now integrate advanced fiber laser engraving, deep 3D debossing, sub-surface heat foil stamping, and custom nickel plate riveting to embed client branding seamlessly into products. Furthermore, batch-level QR code tracking allows distributors to trace raw hide origin and manufacturing dates.
Rooted in Sialkot, Pakistan—the recognized global capital for hand-stitched sporting equipment and master leather crafting—Sedate Group of Industries has operated as an elite OEM & private label manufacturer since 2002. Exporting to over 20 countries across North America, Europe, and Australia, our facility bridges traditional hand-craftsmanship with automated industrial technology.
Selection of top-grade bovine hides, followed by eco-certified vegetable tanning to lock in tensile strength.
Computerized hide splitting ensures exact 10mm or 13mm uniform thickness across all production straps.
Heavy lockstitching with 3-ply nylon thread and installation of solid steel lever locks or dual-prong buckles.
Hand-burnishing, hydrophobic edge sealing, laser logo branding, and barcoded retail carton packaging.
Our integrated production divisions—spanning leather goods, fight gear, and performance apparel—allow global partners to consolidate their supply chain under one roof. Whether you are launching an emerging fitness brand requiring low MOQs (50 pairs per style) or an established international distributor scheduling container-load orders, our 45-day average lead time ensures rapid market readiness.
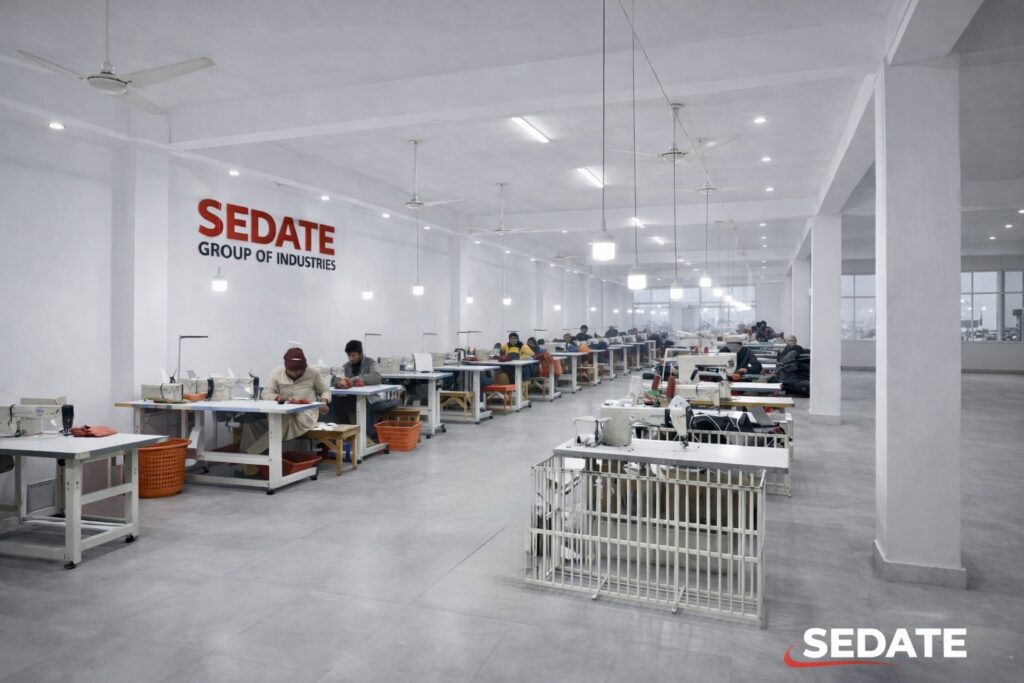
Direct visual evidence of our production floor operations, raw material preparation, stitching lines, and finished quality inspections:
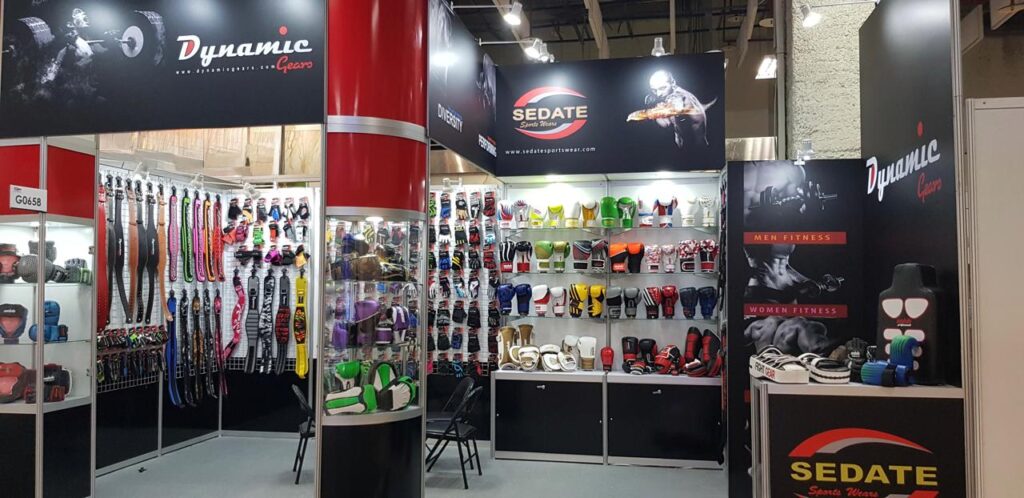
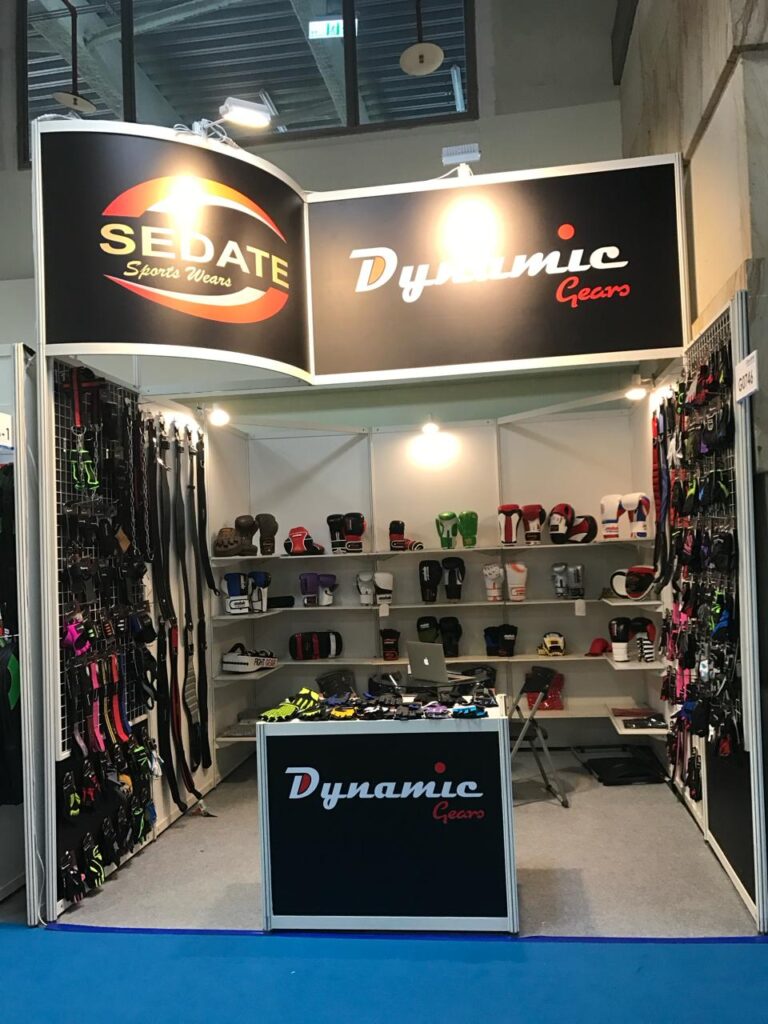
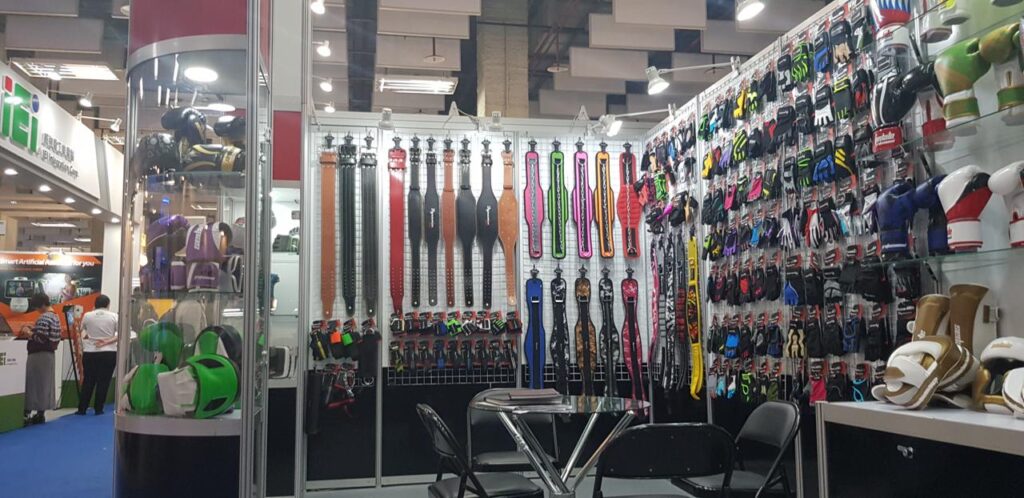
Essential commercial details regarding order volumes, material specs, lead times, and private label customization.
Our standard minimum run starts at 50 units per style and colorway for custom leather belts (including weightlifting lever belts and prong belts). For stitched apparel and sports accessories, standard runs begin at 100 pieces per design. Startup brands can combine multiple size options (S, M, L, XL, XXL) within a single batch order to meet baseline factory tiers.
The 10mm thickness profile offers optimal flexibility and faster break-in time, making it ideal for general strength training, cross-training, and intermediate lifters. The 13mm thickness profile provides maximum intra-abdominal pressure support and rigid brace support required by professional heavy powerlifters. Both options are manufactured strictly to International Powerlifting Federation (IPF) dimensional width standards (4 inches / 10cm wide).
We offer comprehensive OEM private labeling: deep heat debossing, gold/silver foil embossing, fiber laser etching on metal lever buckles, custom woven labels, rubber silicone badges, printed inner suede linings, custom retail boxes, and barcoded hangtags matching your complete brand identity tech pack.
Custom prototype samples are developed within 7 to 12 working days following tech-pack and artwork sign-off. Bulk production averages 45 days from sealed sample approval. Production tracking updates (cutting, stitching, hardware installation, final inspection) are provided weekly by your designated account manager.
We regularly ship door-to-door, FOB, CFR, and CIF shipments to the USA, UK, Canada, Germany, Spain, Australia, Europe, and the Middle East. Our dedicated export logistics team prepares complete documentation, including Commercial Invoices, Packing Lists, Certificates of Origin, and HS-Code classification guidance.
Request a custom quotation, order physical sample prototypes, or schedule a technical consultation with our engineering team today.
Contact Us