Turnkey OEM/ODM solutions engineered for commercial combat academies, fitness franchises, and retail distribution worldwide.
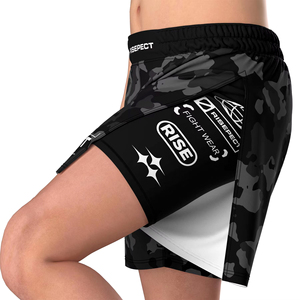
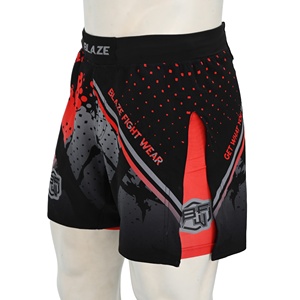
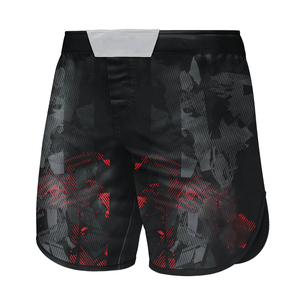
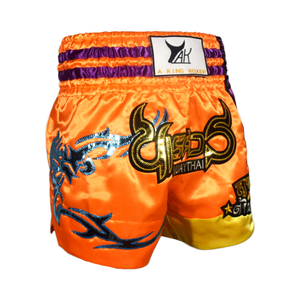
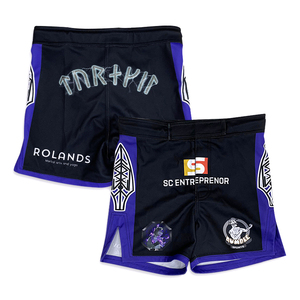
Analysis of structural integrity, kinetic shock dispersion, material stress limits, and industrial production methodologies for high-intensity training environments.
In commercial combat sports facilities, heavy bags absorb tens of thousands of dynamic impacts daily, generating kinetic energy transfers up to 700 Joules per strike. Subpar manufacturing leads to seam tearing, top-strap shearing, and bottom-heavy textile settling.
As a specialized OEM/ODM manufacturer, Sedate Group of Industries implements a 360-degree vector stitching methodology utilizing high-tensile bonded Dacron thread. Stress points are reinforced with double-layered internal webbing and quadruple-stitched X-box anchors, ensuring dynamic force distribution across the entire vertical shell body.
The primary technical flaw in low-grade heavy punching bags is uneven filler settling, which creates hollow upper zones and concrete-hard lower sections. Our proprietary filling technique guarantees uniform tactile response throughout the equipment's lifespan.
We utilize precision-shredded high-density textile matrix combined with a machine-compressed core tube. Surrounding this core is a 25mm high-rebound closed-cell EVA foam liner that cushions impacts, protects athletes' metacarpal structures, and maintains perfect cylindrical symmetry.
Empirical breakdown of shell materials engineered for private label brand positioning and commercial durability requirements.
| Material Shell Grade | Tensile Strength (N/5cm) | Tear Resistance | Abrasion Cycle Life | Recommended Usage Environment | Commercial Tier |
|---|---|---|---|---|---|
| Full-Grain Cowhide Leather (1.4-1.6mm) | > 2,400 N | Ultra-High | 150,000+ Cycles | Elite Pro Academies, World Championship Gyms | Flagship Luxury |
| Engineered Microfiber Leather | > 2,100 N | Ultra-High | 120,000+ Cycles | High-Traffic Commercial Fitness Clubs | Premium Professional |
| High-Tensile Laminated Vinyl / PVC (1000D) | > 1,800 N | High | 80,000+ Cycles | Commercial Combat Gyms, Boxing Clubs | Commercial Standard |
| Heavyweight Poly-Cotton Ripstop Canvas | > 1,400 N | Medium-High | 45,000+ Cycles | BJJ Academies, Home Training Systems | Institutional / Entry |
Key technological advancements transforming combat sports equipment engineering, kinetic design, and athlete interaction.
Modern commercial gyms demand integrated strike analytics. Future heavy bag ODM designs embed internal accelerometer pockets and pressure-conductive internal lining to capture real-time impact velocity, cumulative force (Joules), and strike frequency telemetry without compromising surface tactile integrity.
Standard cylindrical bags are rapidly giving way to specialized biomechanical silhouettes. Teardrop bags, angle uppercut bags, body-opponent shaping, and water-core hybrid systems allow fighters to execute technical knees, hooks, and body strikes with natural kinetic angles.
Global regulatory pressure (such as EU REACH compliance) is accelerating the shift toward solvent-free Polyurethane (PU) and bio-based synthetic leathers. Brands are adopting recycled polyester backing fabrics and non-toxic water-based adhesive formulations to meet eco-label mandates.
Strategic shift in how global fight brands, franchise gyms, and distributors source commercial gear from tier-1 manufacturing hubs.
Leading international combat brands are bypassing trading offices to partner directly with established Sialkot manufacturers. Direct engagement provides full transparency into material bills (BOM), custom pattern ownership, and strict quality assurance compliance.
Modern brand procurement relies on speed-to-market. Brands demand 7-to-12 day rapid prototype turnarounds and flexible pilot MOQs (starting at 50 units for specialized heavy bags or fight gloves) to validate market demand before committing to container-load orders.
With global container shipping rates fluctuating, smart importers source un-filled heavy bag shells packed flat to maximize container cubic capacity (CBM). Unfilled shell importation reduces freight overhead by up to 400% compared to shipping pre-filled units.
Combining 23+ years of Sialkot craftsmanship with modern industrial standard operating procedures.
We offer full brand customization including screen printing, high-density embroidery, 3D logo embossing, laser-etched patch application, custom woven label stitching, and retail-ready barcoded packaging.
Every heavy bag, pair of boxing gloves, or fight short undergoes strict inspection: raw material tensile testing, inline pattern precision auditing, padding density verification, seam strength testing, and final pre-pack inspection.
We export regularly to over 20 countries across North America, Europe, Australia, and the Middle East. Our dedicated export desk handles FOB Sialkot, CFR, CIF, and door-to-door DDP logistics with full customs compliance.
Detailed technical answers for B2B buyers, brand owners, and gym equipment procurement managers.
Our standard OEM production runs start at 50 units per style/colorway for commercial heavy bags, boxing gloves, and protective gear. For stitched performance apparel (rash guards, MMA shorts, compression wear), the MOQ is 100 pieces per style. Emerging brands can split quantities across multiple sizes to meet volume thresholds easily.
Prototype samples are completed within 7 to 12 working days following approval of your tech pack and vector artwork. Bulk production runs average 45 days from sealed pre-production sample sign-off, depending on material complexity, customization techniques, and seasonal order volume.
We supply both options depending on your business model. Importing unfilled heavy bag shells packed flat significantly lowers ocean/air freight costs per unit. However, for regional distributors or turnkey gym orders, we provide pre-filled bags packed with compressed textile matrix and EVA foam liners, fully ready for retail display.
Yes, 100%. We specialize in contract OEM manufacturing. Our pattern engineers work directly with your AI/PDF tech packs, specs sheets, stitching guidelines, color codes (Pantone matching), and custom packaging specifications to ensure identical repeat order replication.
We work with genuine full-grain cowhide leather, ultra-durable microfiber leather, 1000D laminated vinyl (PVC), and heavy poly-cotton ripstop canvas. Shell lining options include 25mm closed-cell EVA foam, shock gel layers, and high-density neoprene backing.
We operate under a strict ISO-aligned quality management framework. Incoming raw materials undergo tensile and tear testing. During assembly, inline inspectors monitor stitch count (SPI), seam reinforcement, and logo positioning. Every order receives a final AQL 2.5 audit prior to master carton sealing.
Elevate your brand's combat equipment line with high-performance manufacturing, precision craftsmanship, and reliable worldwide delivery.